oil mist collector manufacturer
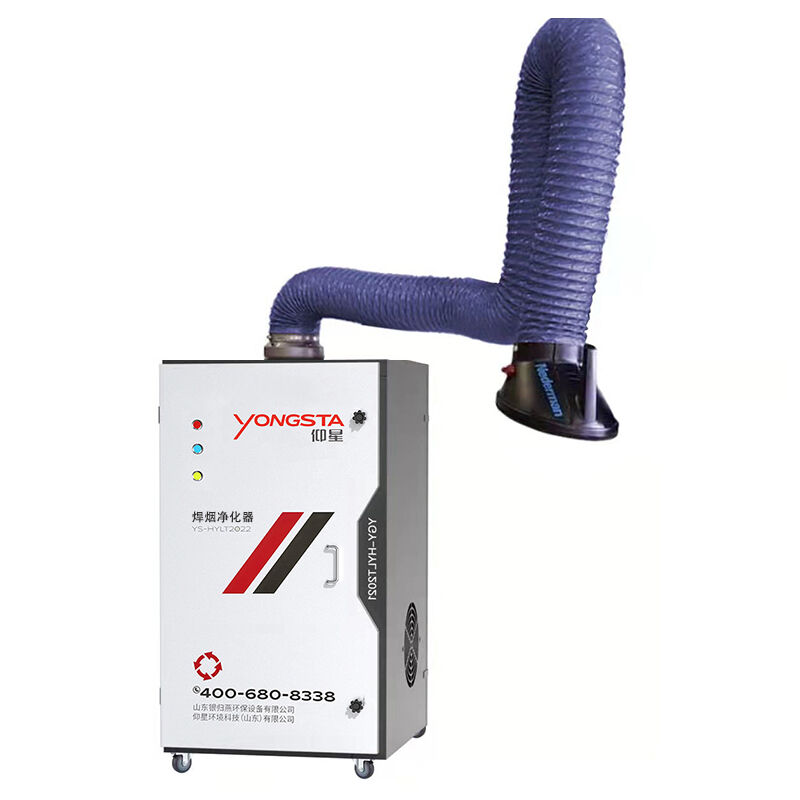
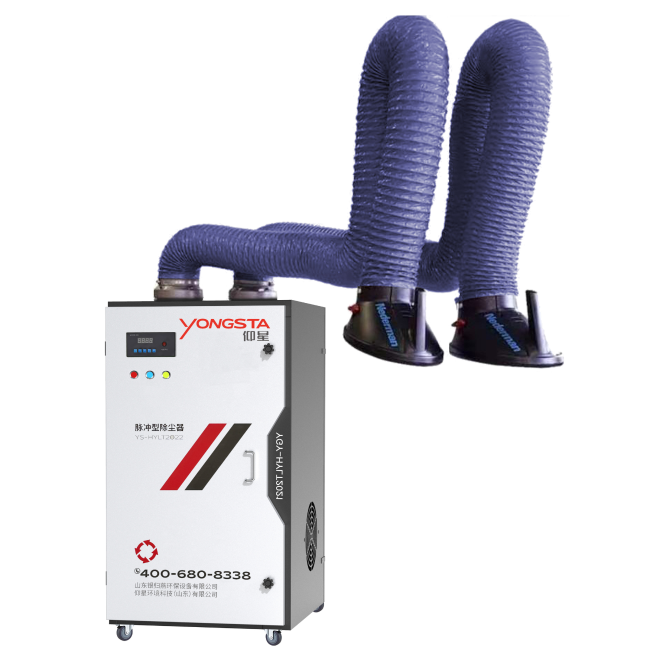
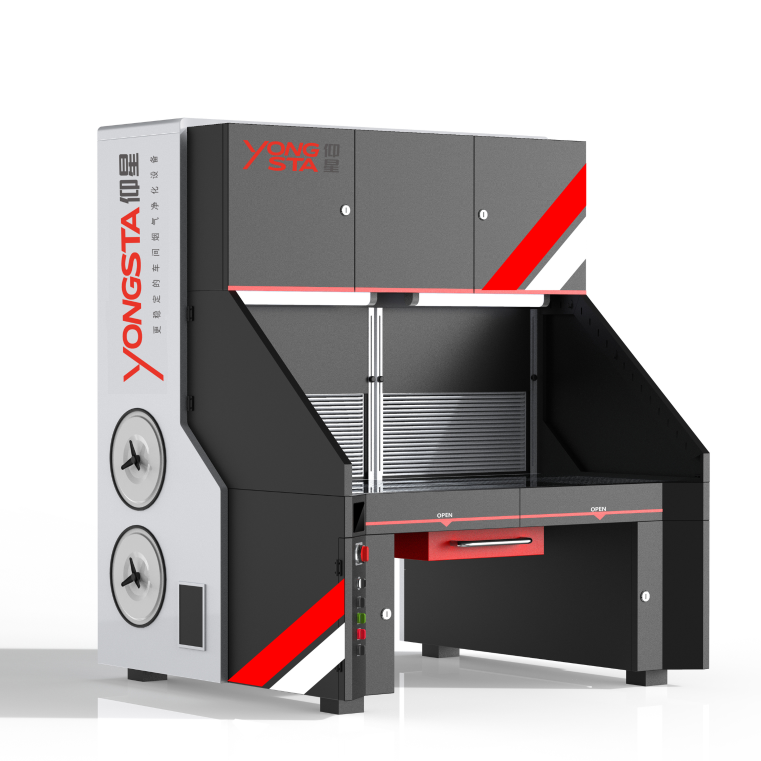
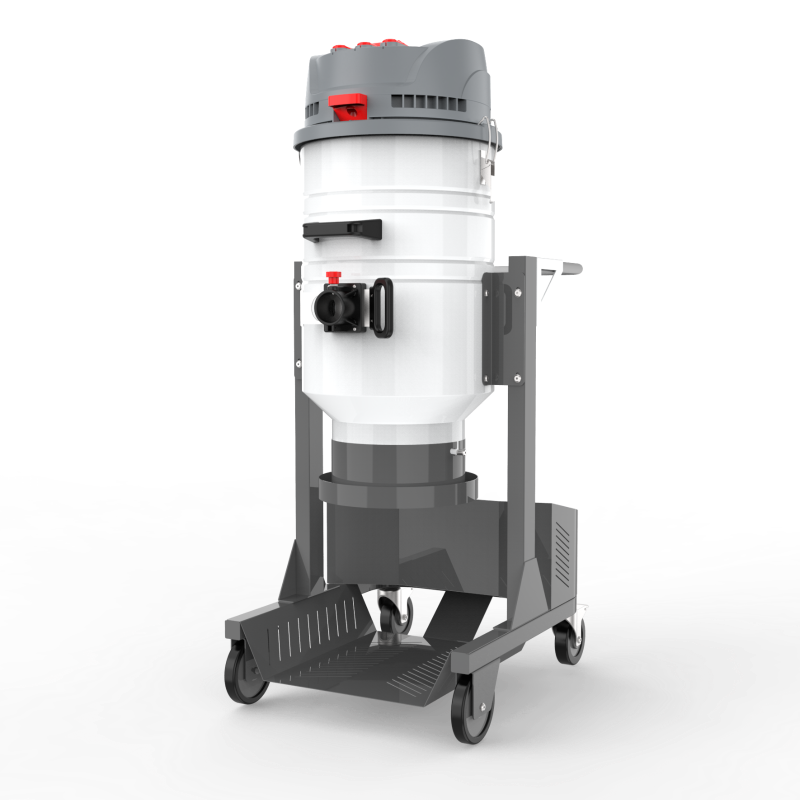
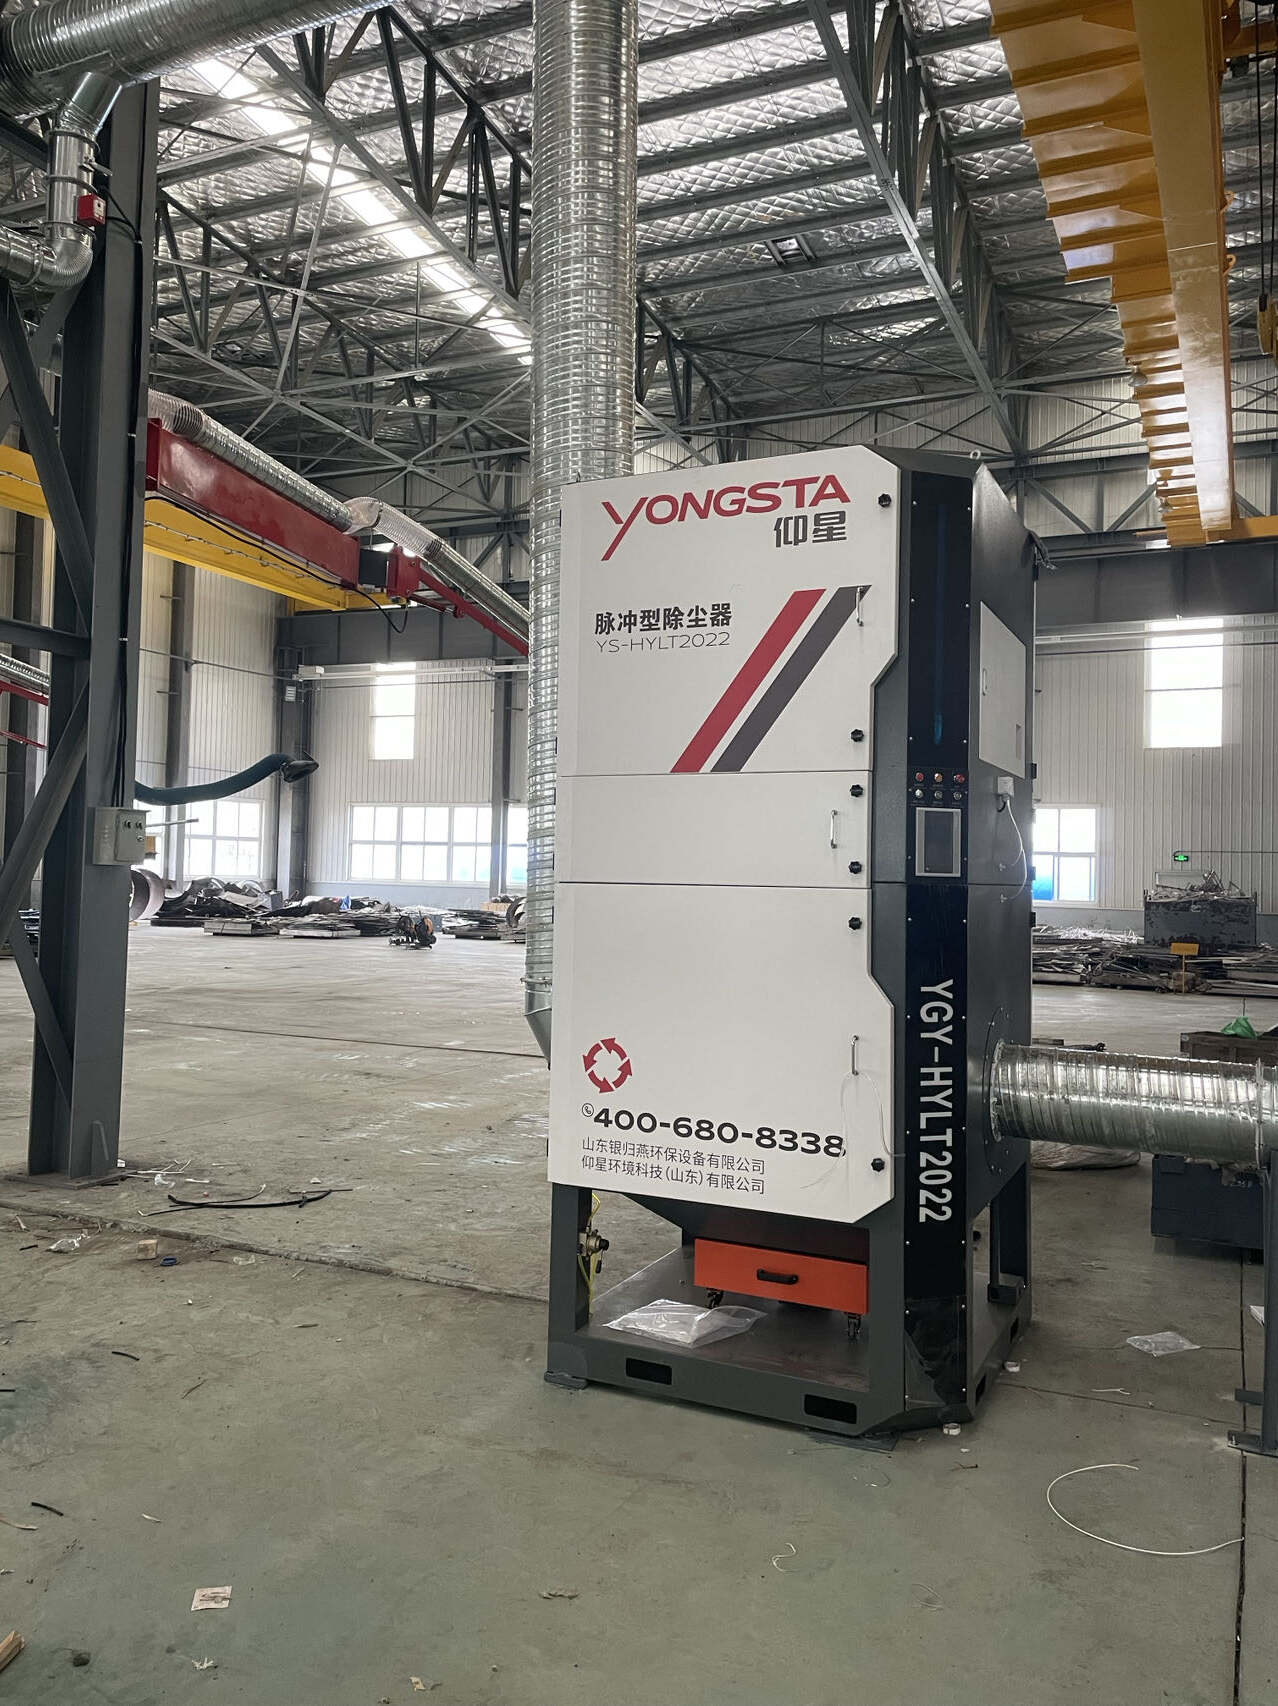
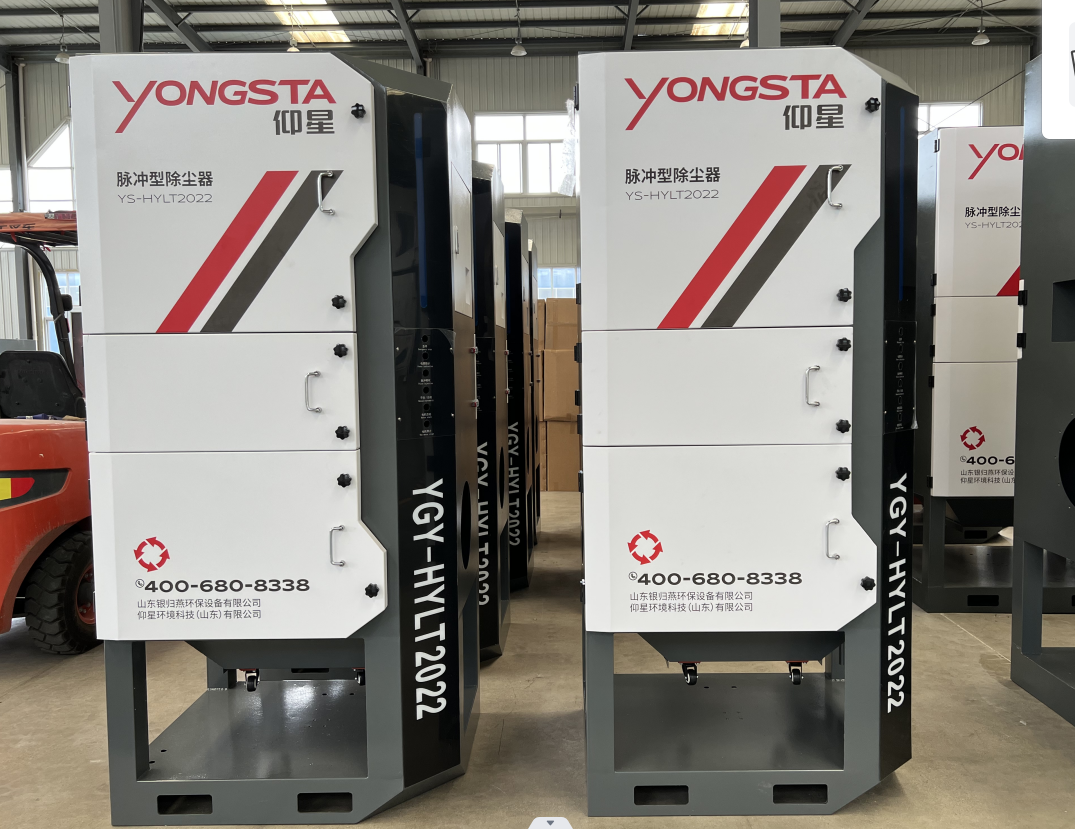
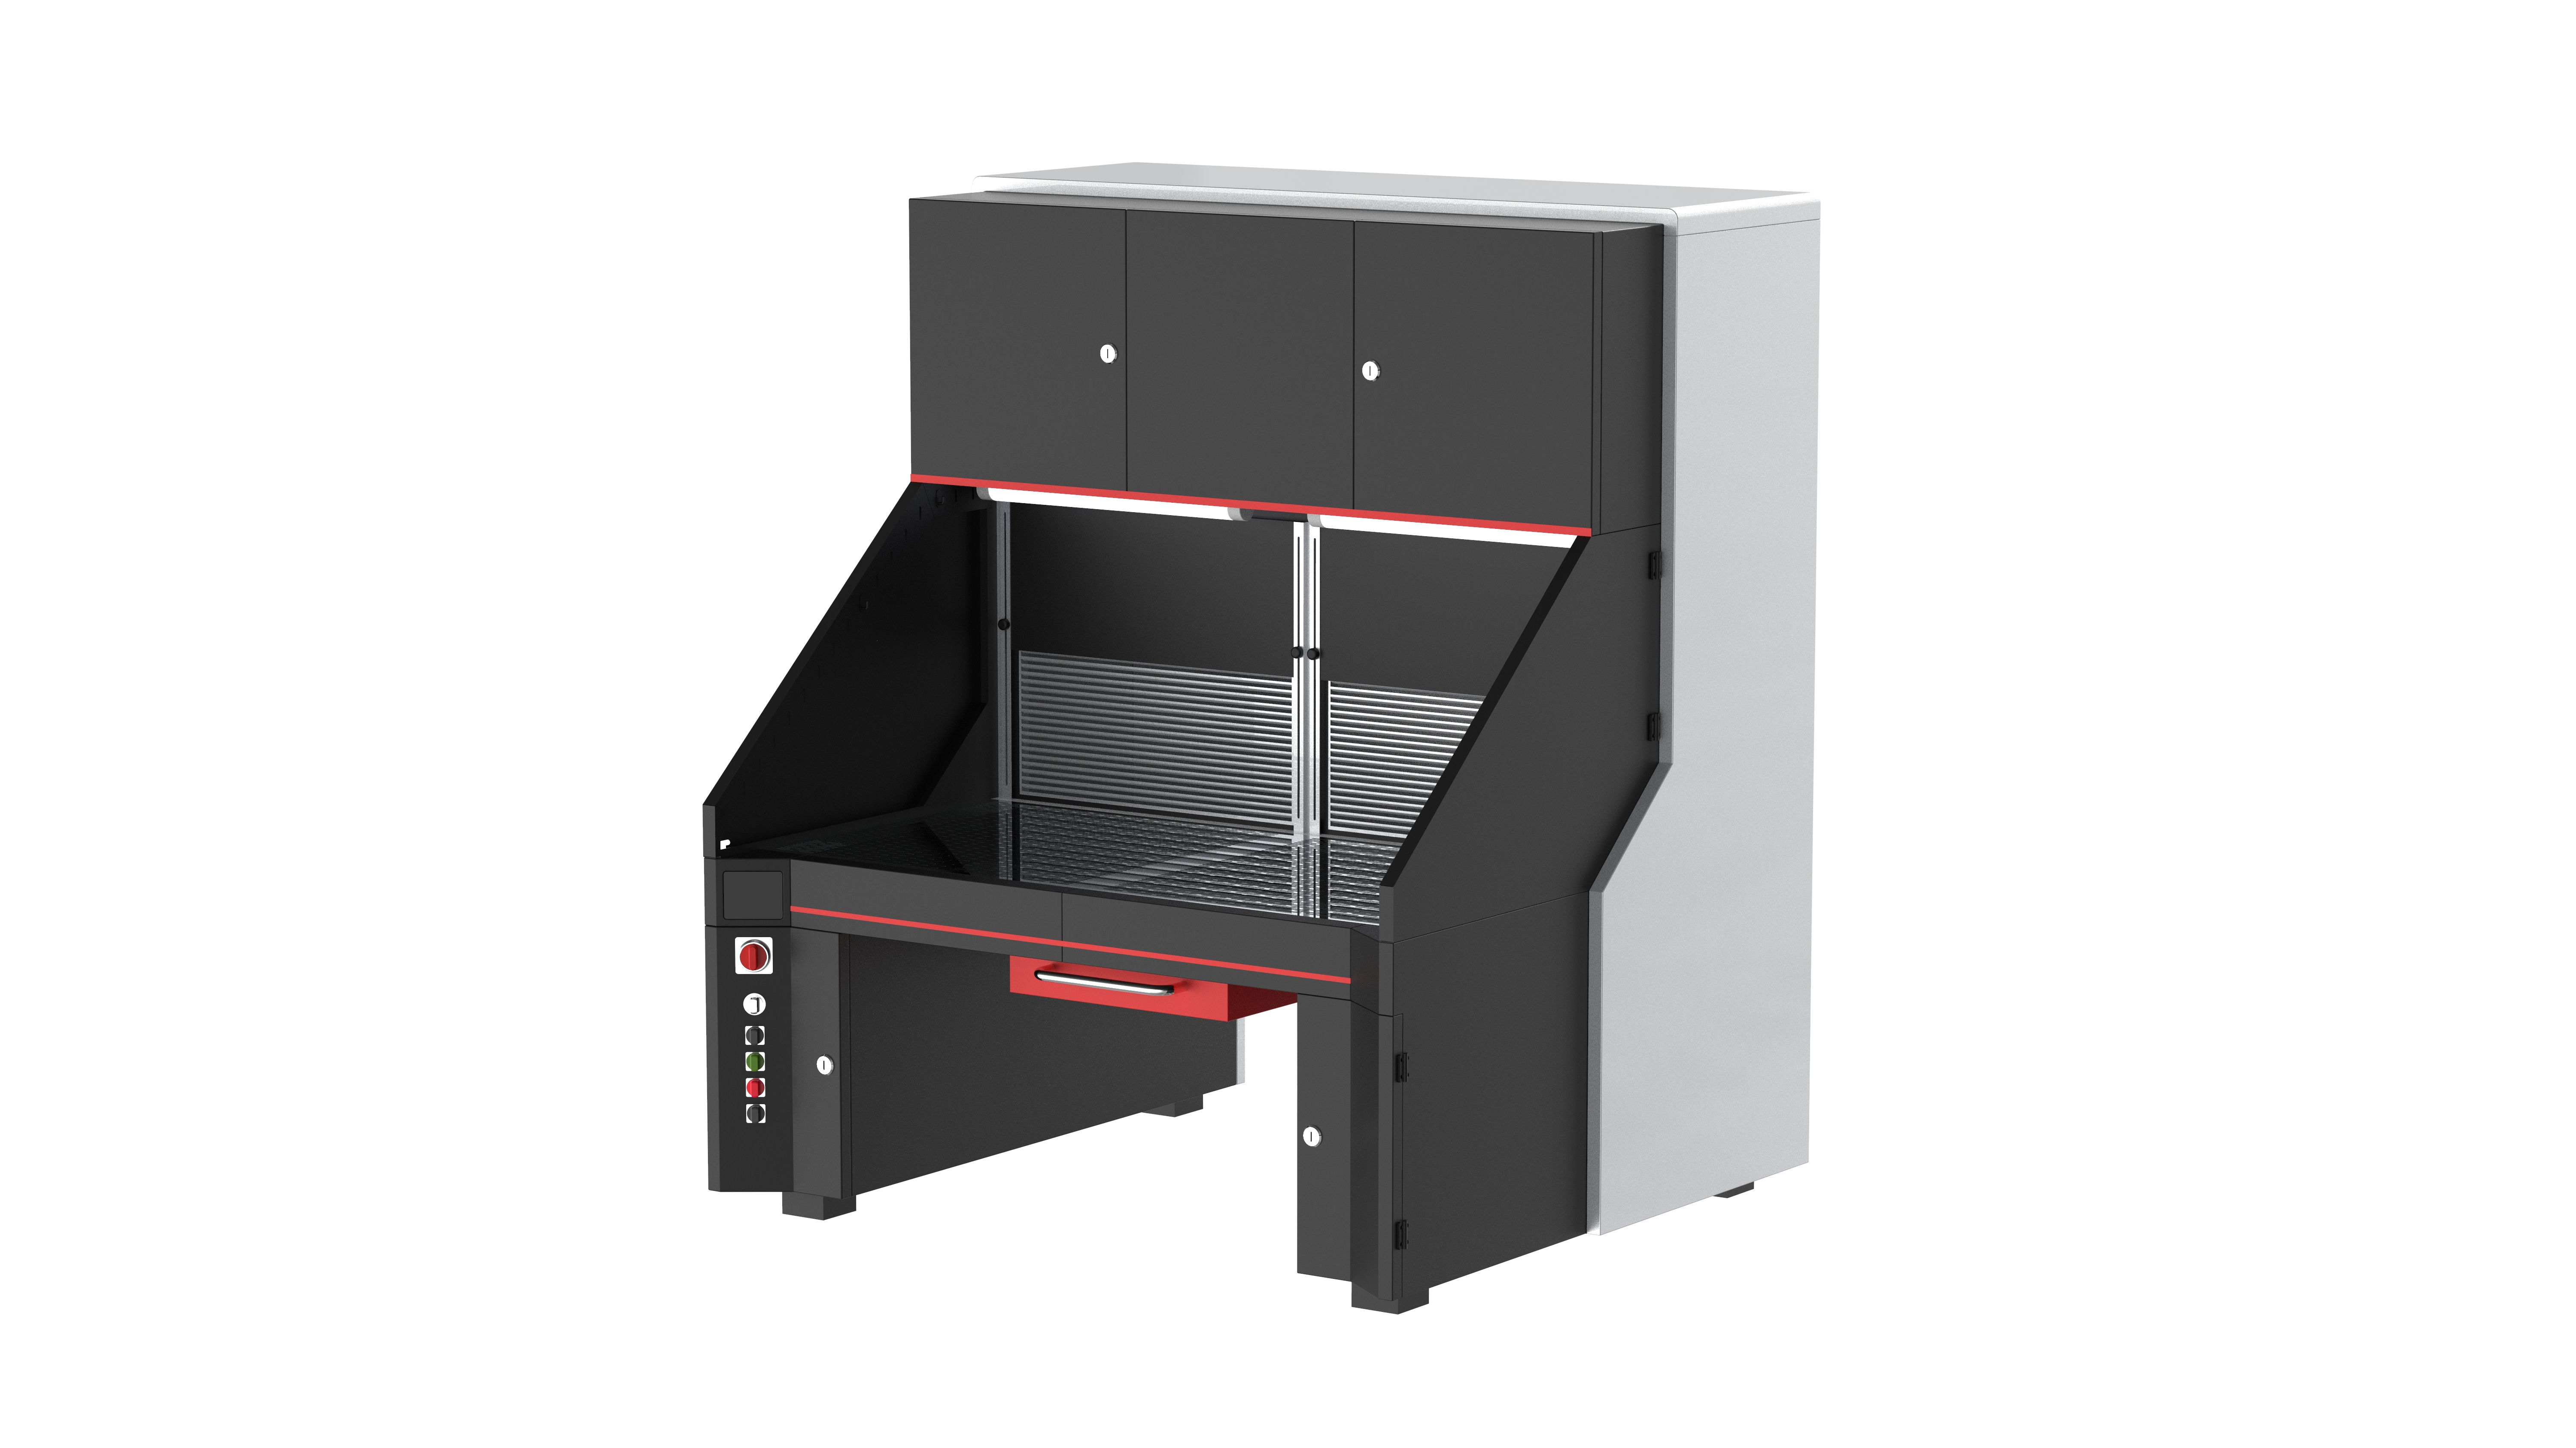
An oil mist collector manufacturer specializes in designing and producing advanced filtration systems that capture and remove airborne oil particles generated during industrial machining operations. These manufacturers create equipment specifically engineered to address the challenges of oil mist, smoke, and coolant vapor that emerge from CNC machines, grinding operations, and metalworking processes. The primary function of these systems involves drawing contaminated air through multi-stage filtration mechanisms that separate oil droplets from the air stream, returning clean air to the workplace environment. Oil mist collector manufacturers employ sophisticated technologies including centrifugal separation, coalescence filtration, and electrostatic precipitation to achieve high-efficiency particle removal. Their products typically feature modular designs that allow customization based on specific production requirements, machine configurations, and facility layouts. These manufacturers understand that different machining operations produce varying particle sizes and concentrations, requiring tailored solutions. The technological features integrated into modern oil mist collectors include variable speed controls, automatic filter monitoring systems, and energy-efficient motors that reduce operational costs. Applications span across automotive manufacturing, aerospace component production, medical device fabrication, and general metalworking facilities where precision machining generates significant oil mist. The equipment protects both worker health and machinery longevity by preventing oil accumulation on surfaces and reducing respiratory hazards. Leading oil mist collector manufacturers invest heavily in research and development to improve collection efficiency, reduce maintenance requirements, and minimize energy consumption. They provide comprehensive support including installation guidance, performance optimization, and ongoing technical assistance. The manufacturing process itself involves precision engineering, quality control testing, and compliance with international safety standards. These manufacturers recognize that effective oil mist collection directly impacts production quality, workplace safety, and environmental compliance, making their role critical in modern manufacturing environments.
 ×






 EN