Industrial Vacuum Systems for Dust - Professional Dust Collection Solutions for Manufacturing

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

industrial vacuum systems for dust

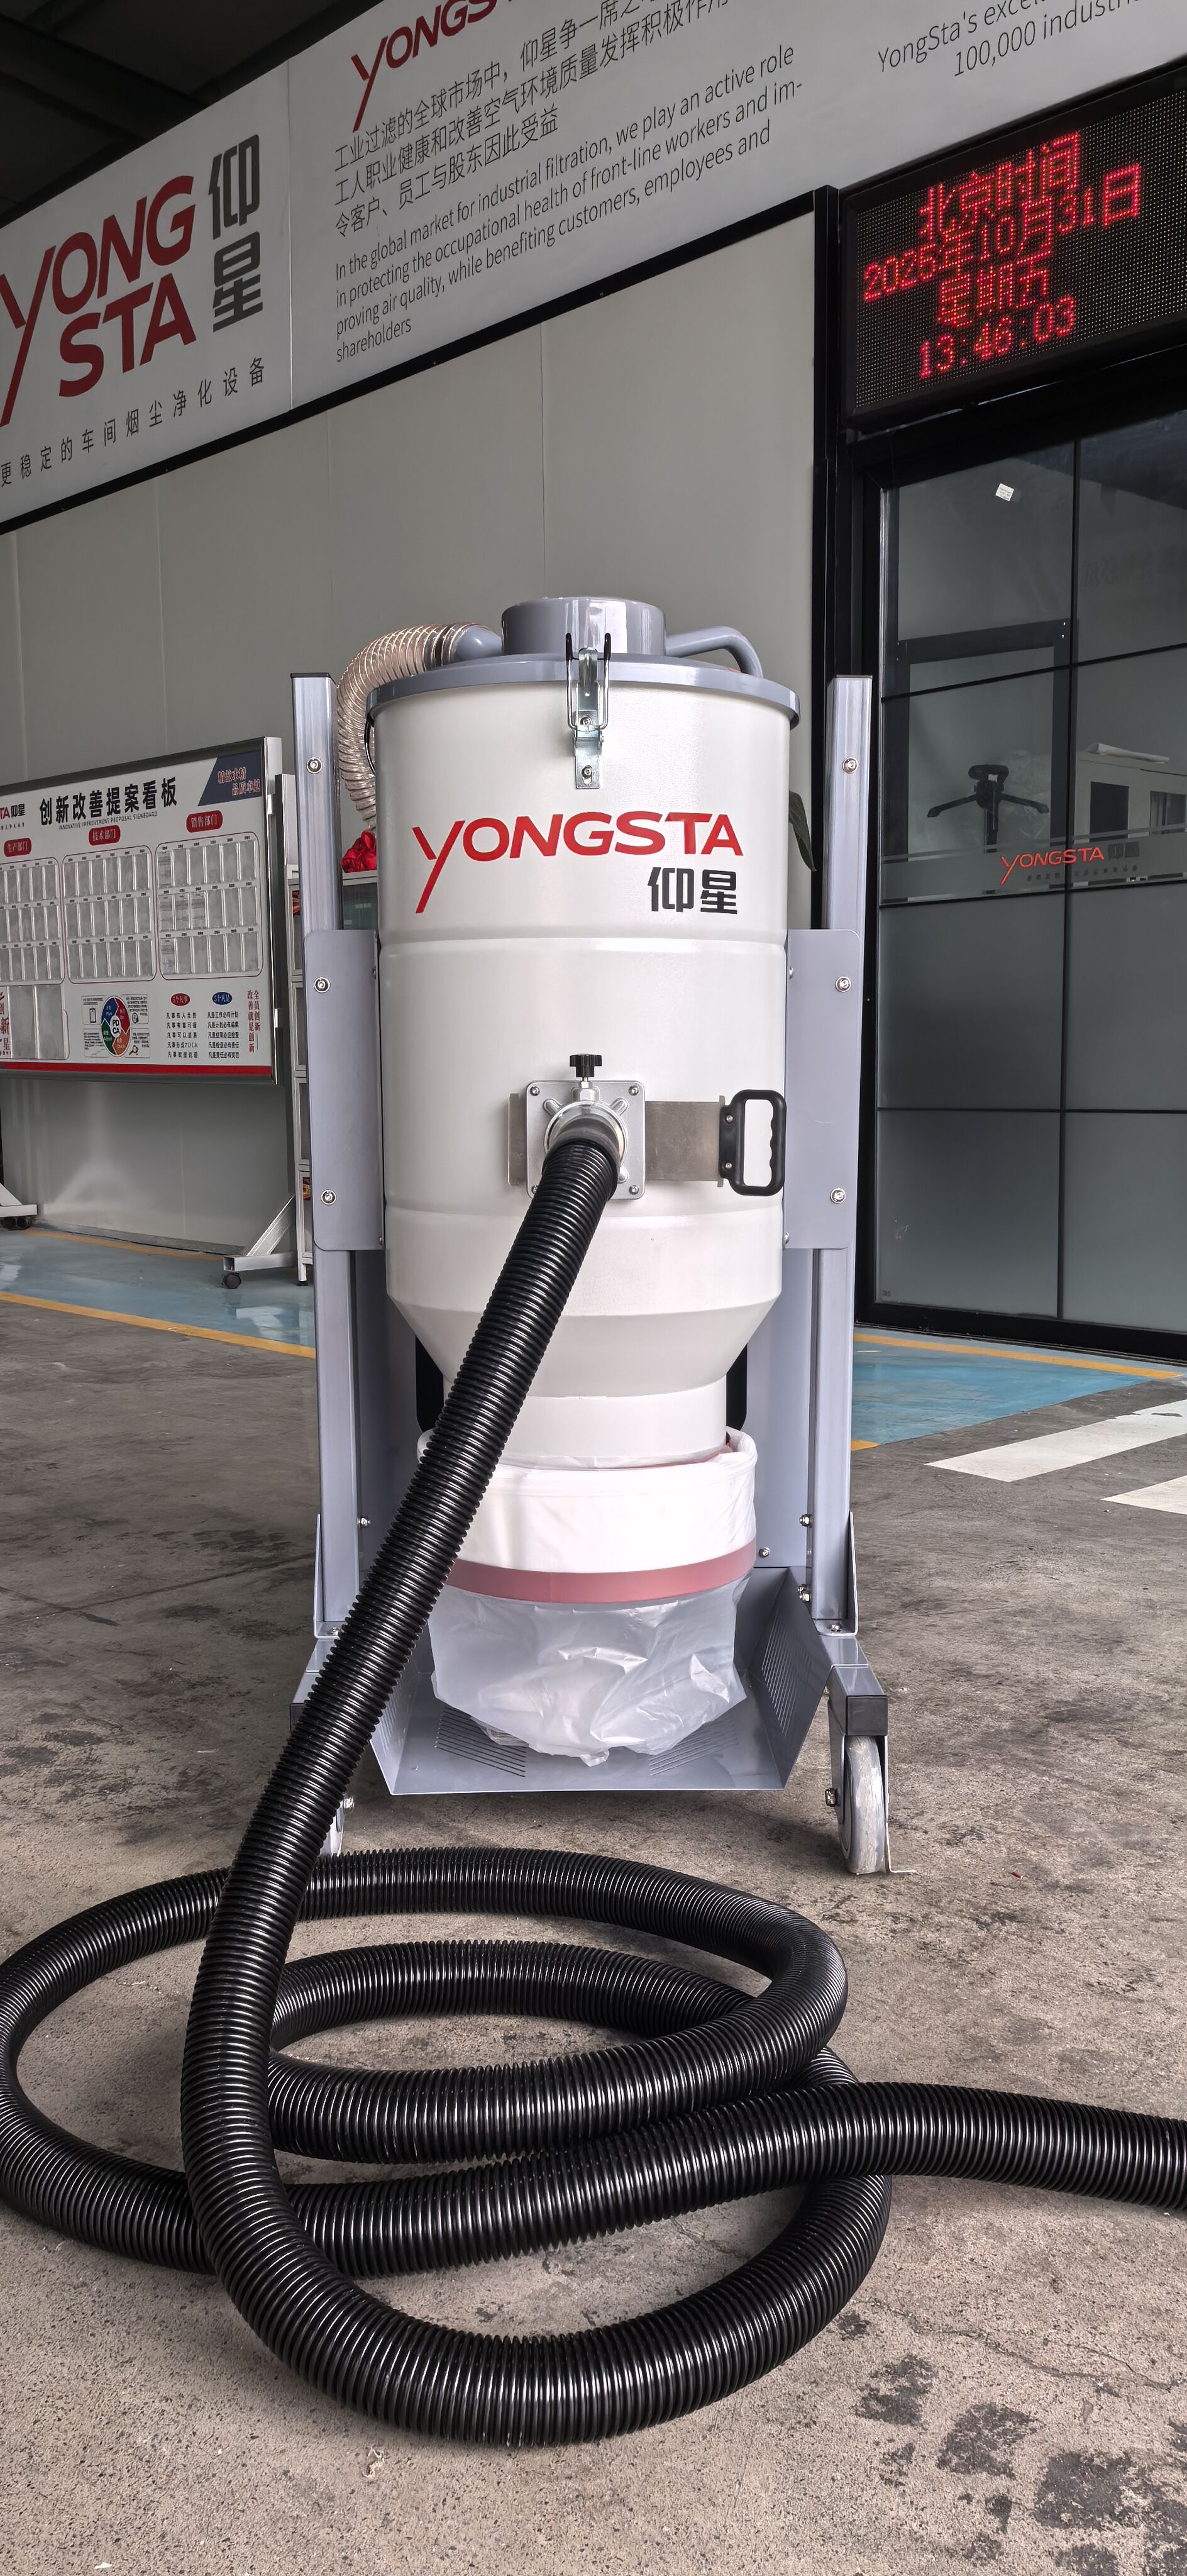
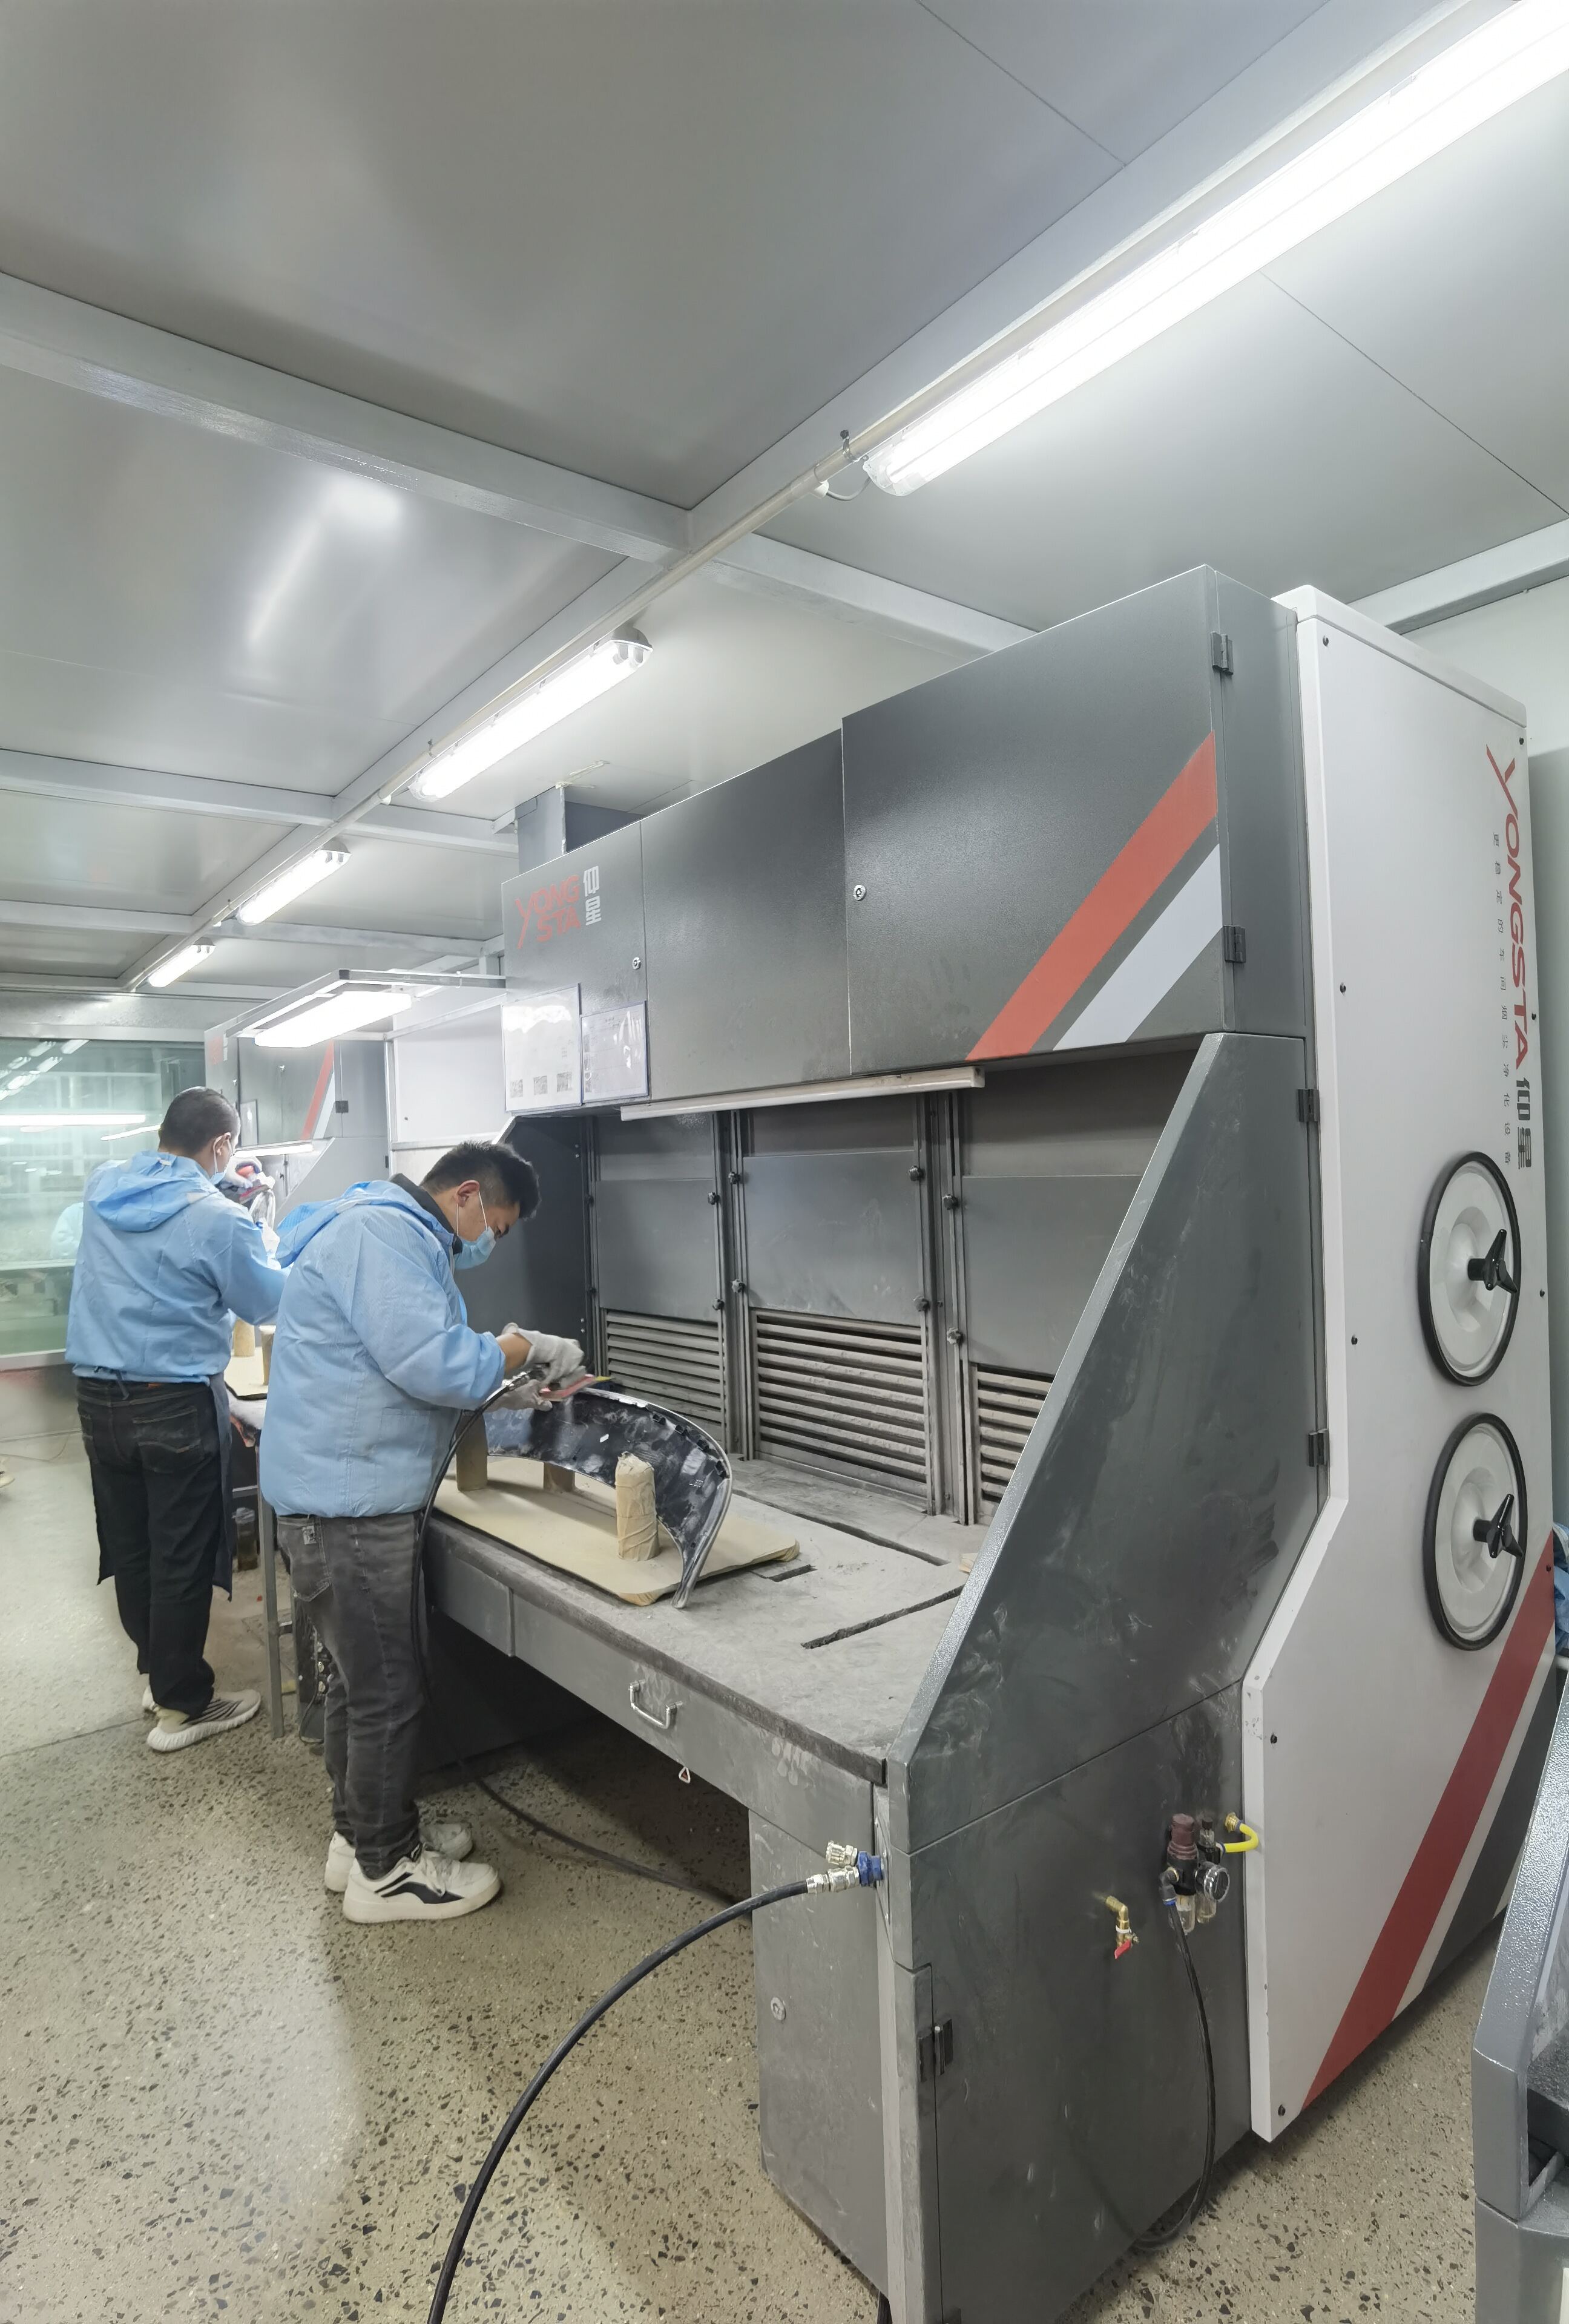
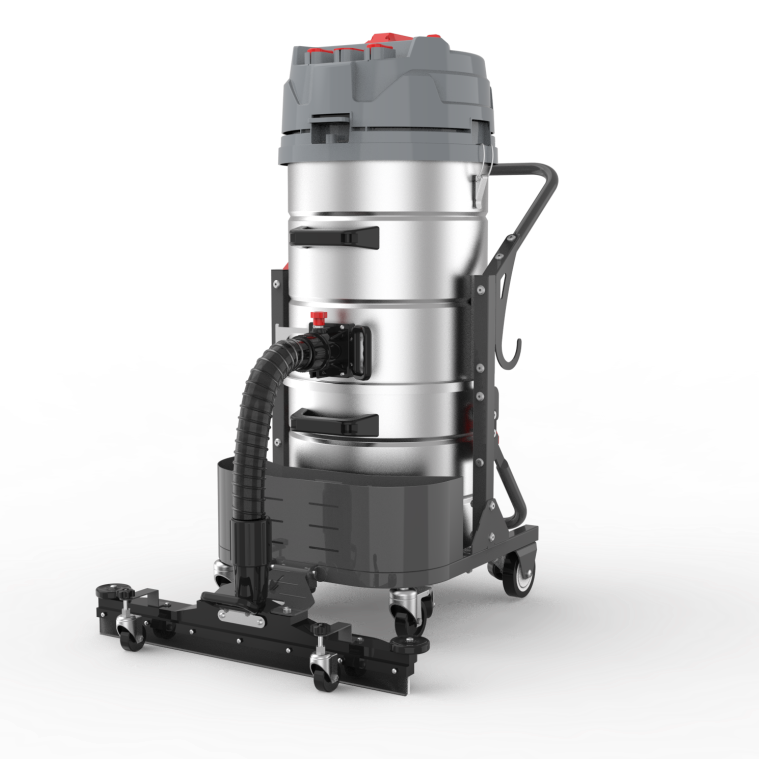
Industrial vacuum systems for dust represent a critical solution for maintaining clean, safe, and compliant work environments across manufacturing facilities, workshops, and production plants. These specialized systems are engineered to capture, contain, and remove airborne particulates, debris, and hazardous dust materials that accumulate during various industrial processes. Unlike standard commercial vacuums, industrial vacuum systems for dust are built with robust components designed to handle continuous operation, high volumes of material, and challenging environmental conditions. The main functions of these systems include effective dust collection at the source, filtration of harmful particles to protect worker health, and prevention of dust accumulation that could lead to equipment damage or fire hazards. Modern industrial vacuum systems for dust incorporate advanced cyclonic separation technology, multi-stage filtration processes, and powerful suction capabilities that can handle everything from fine powders to heavy debris. These systems typically feature large-capacity collection bins or drums, reducing the frequency of emptying and minimizing operational interruptions. The technological features often include HEPA filtration for capturing particles as small as 0.3 microns, automatic filter cleaning mechanisms to maintain consistent suction power, and explosion-proof designs for facilities handling combustible dust. Applications span numerous industries including metalworking, woodworking, pharmaceutical manufacturing, food processing, chemical production, and construction. In metalworking shops, industrial vacuum systems for dust remove metal shavings and grinding dust. Woodworking facilities rely on these systems to capture sawdust and wood particles. Pharmaceutical and food processing plants use them to maintain sterile environments and prevent cross-contamination. The versatility of industrial vacuum systems for dust makes them indispensable for any operation where dust generation poses risks to product quality, worker safety, or regulatory compliance. These systems can be configured as portable units for flexibility or installed as centralized networks serving multiple workstations throughout a facility.

New Product Recommendations

Investing in industrial vacuum systems for dust delivers substantial practical benefits that directly impact your bottom line and operational efficiency. First and foremost, these systems dramatically improve workplace safety by removing hazardous dust particles that can cause respiratory problems, allergic reactions, and long-term health issues for your employees. Clean air means healthier workers, which translates to reduced sick days, lower insurance costs, and improved morale. Beyond health benefits, industrial vacuum systems for dust protect your valuable equipment and machinery from premature wear and failure. Dust accumulation on motors, bearings, and electronic components accelerates deterioration and causes costly breakdowns. By keeping your facility clean, you extend equipment lifespan and reduce maintenance expenses. Regulatory compliance becomes straightforward when you implement proper dust collection. OSHA and EPA regulations mandate specific air quality standards, and industrial vacuum systems for dust help you meet these requirements effortlessly, avoiding hefty fines and potential shutdowns. The productivity gains are equally impressive. Workers spend less time on manual cleaning tasks and more time on value-adding activities. Clean workspaces also improve visibility and reduce accidents caused by slippery floors or obscured hazards. Product quality sees measurable improvement as well. Dust contamination ruins finishes, causes defects, and leads to customer complaints and returns. Industrial vacuum systems for dust eliminate these quality issues, protecting your reputation and reducing waste. Energy efficiency is another advantage often overlooked. Modern systems use optimized airflow designs and variable speed motors that consume less power while delivering superior performance. The initial investment pays for itself through reduced energy bills over the system's lifetime. Fire and explosion prevention cannot be understated, especially in facilities handling combustible materials like wood dust, metal powders, or chemical compounds. Industrial vacuum systems for dust with proper grounding and spark-resistant construction eliminate ignition sources and safely contain flammable particles. Flexibility in system design means you can start with a basic setup and expand as your needs grow. Modular components allow for easy upgrades and reconfigurations without replacing the entire system. Noise reduction features in premium industrial vacuum systems for dust create a more comfortable work environment, reducing stress and improving communication among team members. The return on investment becomes evident within months as you experience fewer disruptions, lower operating costs, and enhanced productivity across all departments.

Latest News

Yongsta R&D Team Wins 3 Dust Removal Technology Patents, Leading Industry Innovation

09

Apr

Yongsta R&D Team Wins 3 Dust Removal Technology Patents, Leading Industry Innovation

View More
Yongsta Cooperates with TUV for ATEX Explosion-Proof Certification, Explosion-Proof Dust Collector to Be Launched Soon

09

Apr

Yongsta Cooperates with TUV for ATEX Explosion-Proof Certification, Explosion-Proof Dust Collector to Be Launched Soon

View More
Empowering Benchmark Manufacturing! Yongsta Cartridge Dust Collector Aids Siemens Transformer China Factory's Dust Removal Renovation and Gains High Recognition

09

Apr

Empowering Benchmark Manufacturing! Yongsta Cartridge Dust Collector Aids Siemens Transformer China Factory's Dust Removal Renovation and Gains High Recognition

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

industrial vacuum systems for dust

Advanced Multi-Stage Filtration Technology Ensures Maximum Air Purity

Advanced Multi-Stage Filtration Technology Ensures Maximum Air Purity

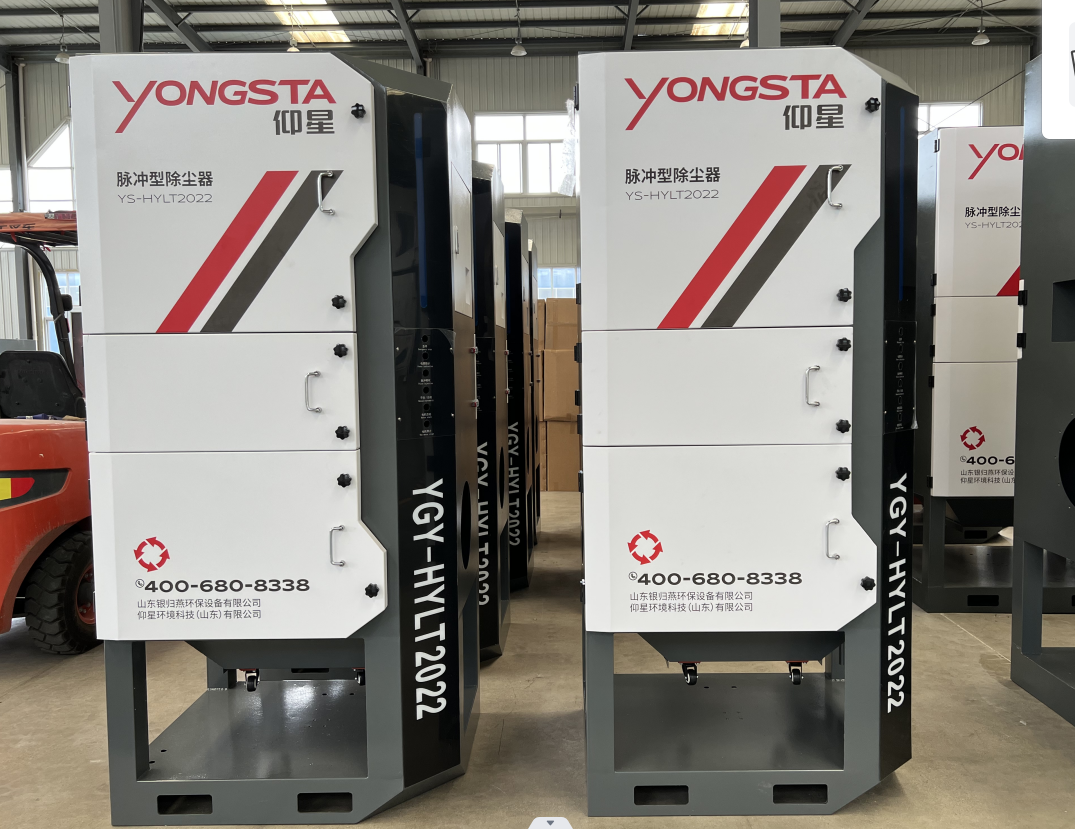
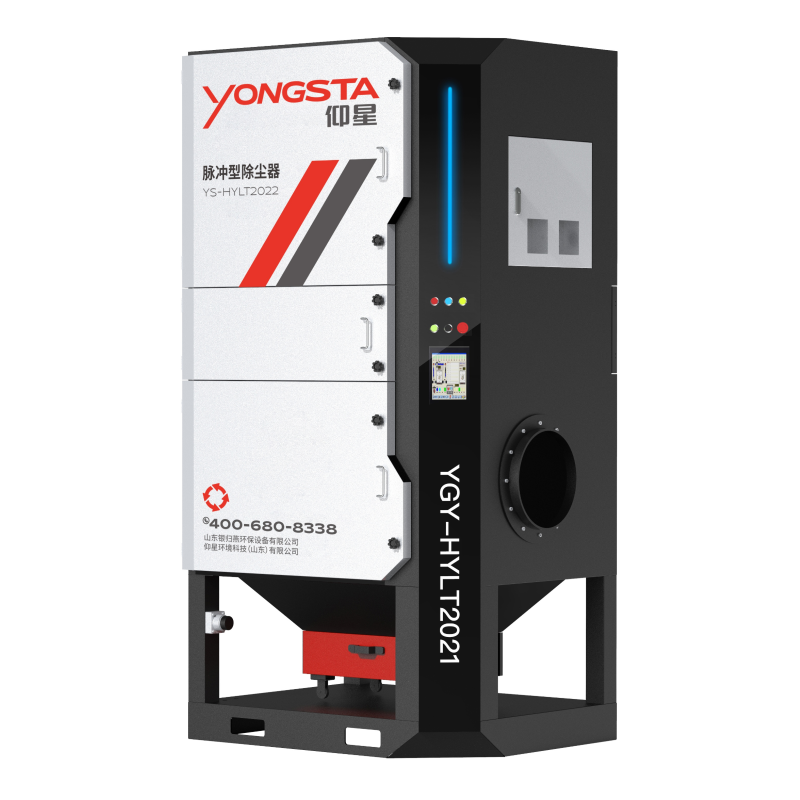
The filtration capability of industrial vacuum systems for dust stands as perhaps their most critical feature, directly determining both worker safety and system effectiveness. Modern systems employ sophisticated multi-stage filtration processes that capture particles across the entire size spectrum, from large debris down to submicron contaminants. The first stage typically involves a cyclonic separator or pre-filter that removes larger particles through centrifugal force, preventing them from reaching the main filter and extending its service life. This initial separation handles approximately 80 to 90 percent of collected material by volume, significantly reducing the load on downstream filters. The second stage features high-efficiency particulate filters, often HEPA-rated, capable of trapping 99.97 percent of particles measuring 0.3 microns or larger. This level of filtration is essential for facilities dealing with toxic substances, allergens, or materials requiring stringent contamination control. Some industrial vacuum systems for dust incorporate additional activated carbon filters for capturing odors and volatile organic compounds, making them suitable for chemical processing environments. The filtration technology in these systems includes automatic cleaning mechanisms such as pulse-jet systems that periodically blast compressed air through filters in reverse, dislodging accumulated dust back into the collection container. This self-cleaning capability maintains consistent suction power throughout operation and dramatically extends filter life compared to manual cleaning methods. Filter monitoring systems with pressure differential gauges alert operators when filters require attention, preventing performance degradation and potential system damage. The housing design ensures proper sealing to prevent bypass, where unfiltered air escapes around filter edges. Industrial vacuum systems for dust with tool-less filter access allow quick replacements during maintenance windows, minimizing downtime. The investment in superior filtration pays dividends through compliance with air quality regulations, protection of worker health, and prevention of dust re-circulation that would otherwise settle on clean surfaces. For industries handling silica, asbestos, or other regulated materials, the filtration performance of industrial vacuum systems for dust is not just a convenience but a legal requirement that protects your business from liability and ensures ethical treatment of your workforce.
Robust Construction and Continuous-Duty Performance for Demanding Industrial Environments

Robust Construction and Continuous-Duty Performance for Demanding Industrial Environments

Industrial vacuum systems for dust are engineered with heavy-duty construction that withstands the punishing conditions of manufacturing and production environments where standard equipment would quickly fail. The durability begins with the housing materials, typically fabricated from thick-gauge steel or stainless steel that resists dents, corrosion, and impact damage from forklifts, falling objects, and daily wear. Powder-coated finishes provide additional protection against chemicals, moisture, and abrasive materials common in industrial settings. The motor assemblies in industrial vacuum systems for dust are specifically designed for continuous operation, featuring thermal overload protection, sealed bearings, and cooling systems that prevent overheating during extended use. Unlike consumer-grade vacuums rated for intermittent duty cycles, these industrial units can run eight hours or more without rest, making them suitable for integration into production lines and automated processes. The suction power remains consistent even when collection containers approach capacity, thanks to efficient airflow designs and powerful turbines that generate substantial negative pressure. Hose and attachment durability matches the main unit quality, with reinforced construction, abrasion-resistant materials, and secure connections that prevent separation during use. Industrial vacuum systems for dust often feature larger diameter hoses, typically ranging from two to four inches, allowing higher material flow rates and reducing clogging incidents. The wheels and casters on portable units are industrial-grade, with capacities exceeding the loaded weight of the system and materials designed to roll smoothly across rough concrete floors, metal grating, and uneven surfaces. Electrical components meet stringent safety standards with proper grounding, strain relief on power cords, and switches rated for the electrical loads involved. For hazardous locations, explosion-proof industrial vacuum systems for dust incorporate specialized motors, grounded components, and conductive hoses that dissipate static electricity, preventing sparks that could ignite combustible dust. The collection containers are designed for easy emptying with features like quick-release latches, dump valves, or bag-out systems that contain dust during disposal. Maintenance accessibility is built into the design, with service panels, clear labeling, and modular components that technicians can replace without specialized tools. This robust construction ensures that industrial vacuum systems for dust deliver reliable performance year after year, with total cost of ownership far lower than repeatedly replacing inadequate equipment.

Customizable Configurations and Scalable Solutions for Every Application

Customizable Configurations and Scalable Solutions for Every Application

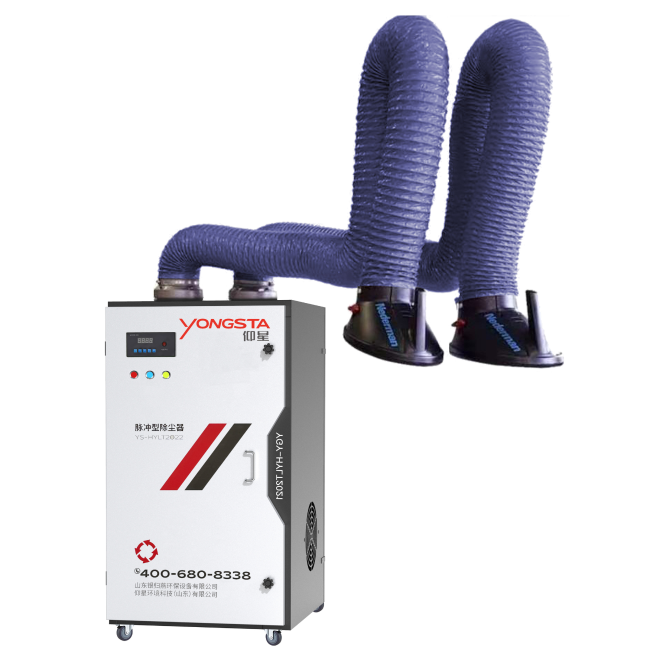
The versatility of industrial vacuum systems for dust lies in their ability to be tailored precisely to your specific operational requirements, facility layout, and material handling needs. Manufacturers offer extensive customization options that transform these systems from generic equipment into optimized solutions for your unique challenges. Portable units provide maximum flexibility for facilities with multiple work areas or changing production layouts, allowing operators to move suction power wherever needed. These mobile industrial vacuum systems for dust typically feature compact footprints, ergonomic handles, and robust wheels that navigate tight spaces and crowded shop floors. For permanent installations, centralized systems serve multiple workstations through a network of piping and strategically placed inlets, eliminating the need for individual units at each location. This approach reduces capital costs, simplifies maintenance, and ensures consistent performance across the facility. The piping can be routed overhead, through walls, or under floors depending on your building structure and aesthetic preferences. Suction power can be adjusted through blast gates or automated dampers that direct airflow to active workstations while closing off unused branches. Industrial vacuum systems for dust are available in various power ratings, from small units handling single machines to massive installations serving entire production halls. Collection capacity ranges from compact drums suitable for intermittent use to large hoppers and silos that store thousands of pounds of material between emptying cycles. For operations generating valuable materials like precious metal dust or recyclable plastics, recovery systems can be integrated to separate and collect these materials for reuse or resale. Automation capabilities include integration with machine controls so the vacuum activates automatically when equipment starts, ensuring dust capture without operator intervention. Remote monitoring systems provide real-time data on filter condition, collection levels, and system performance, enabling predictive maintenance and preventing unexpected failures. Specialized attachments expand functionality, with options including crevice tools for tight spaces, wide floor nozzles for large areas, and custom-designed hoods that mount directly to machinery for source capture. Industrial vacuum systems for dust can be specified with features like spark arrestors for metalworking applications, grounded components for explosive atmospheres, and washdown-rated enclosures for food processing environments. The scalability means you can start with a basic system and add capacity, filtration stages, or additional pickup points as your operation grows, protecting your initial investment while accommodating expansion. This customization ensures that industrial vacuum systems for dust deliver optimal performance for your specific materials, production processes, and facility constraints rather than forcing you to adapt your operations to equipment limitations.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
email goToTop