Cartridge Filter Dust Collector: High-Efficiency Industrial Air Filtration Systems

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

cartridge filter dust collector

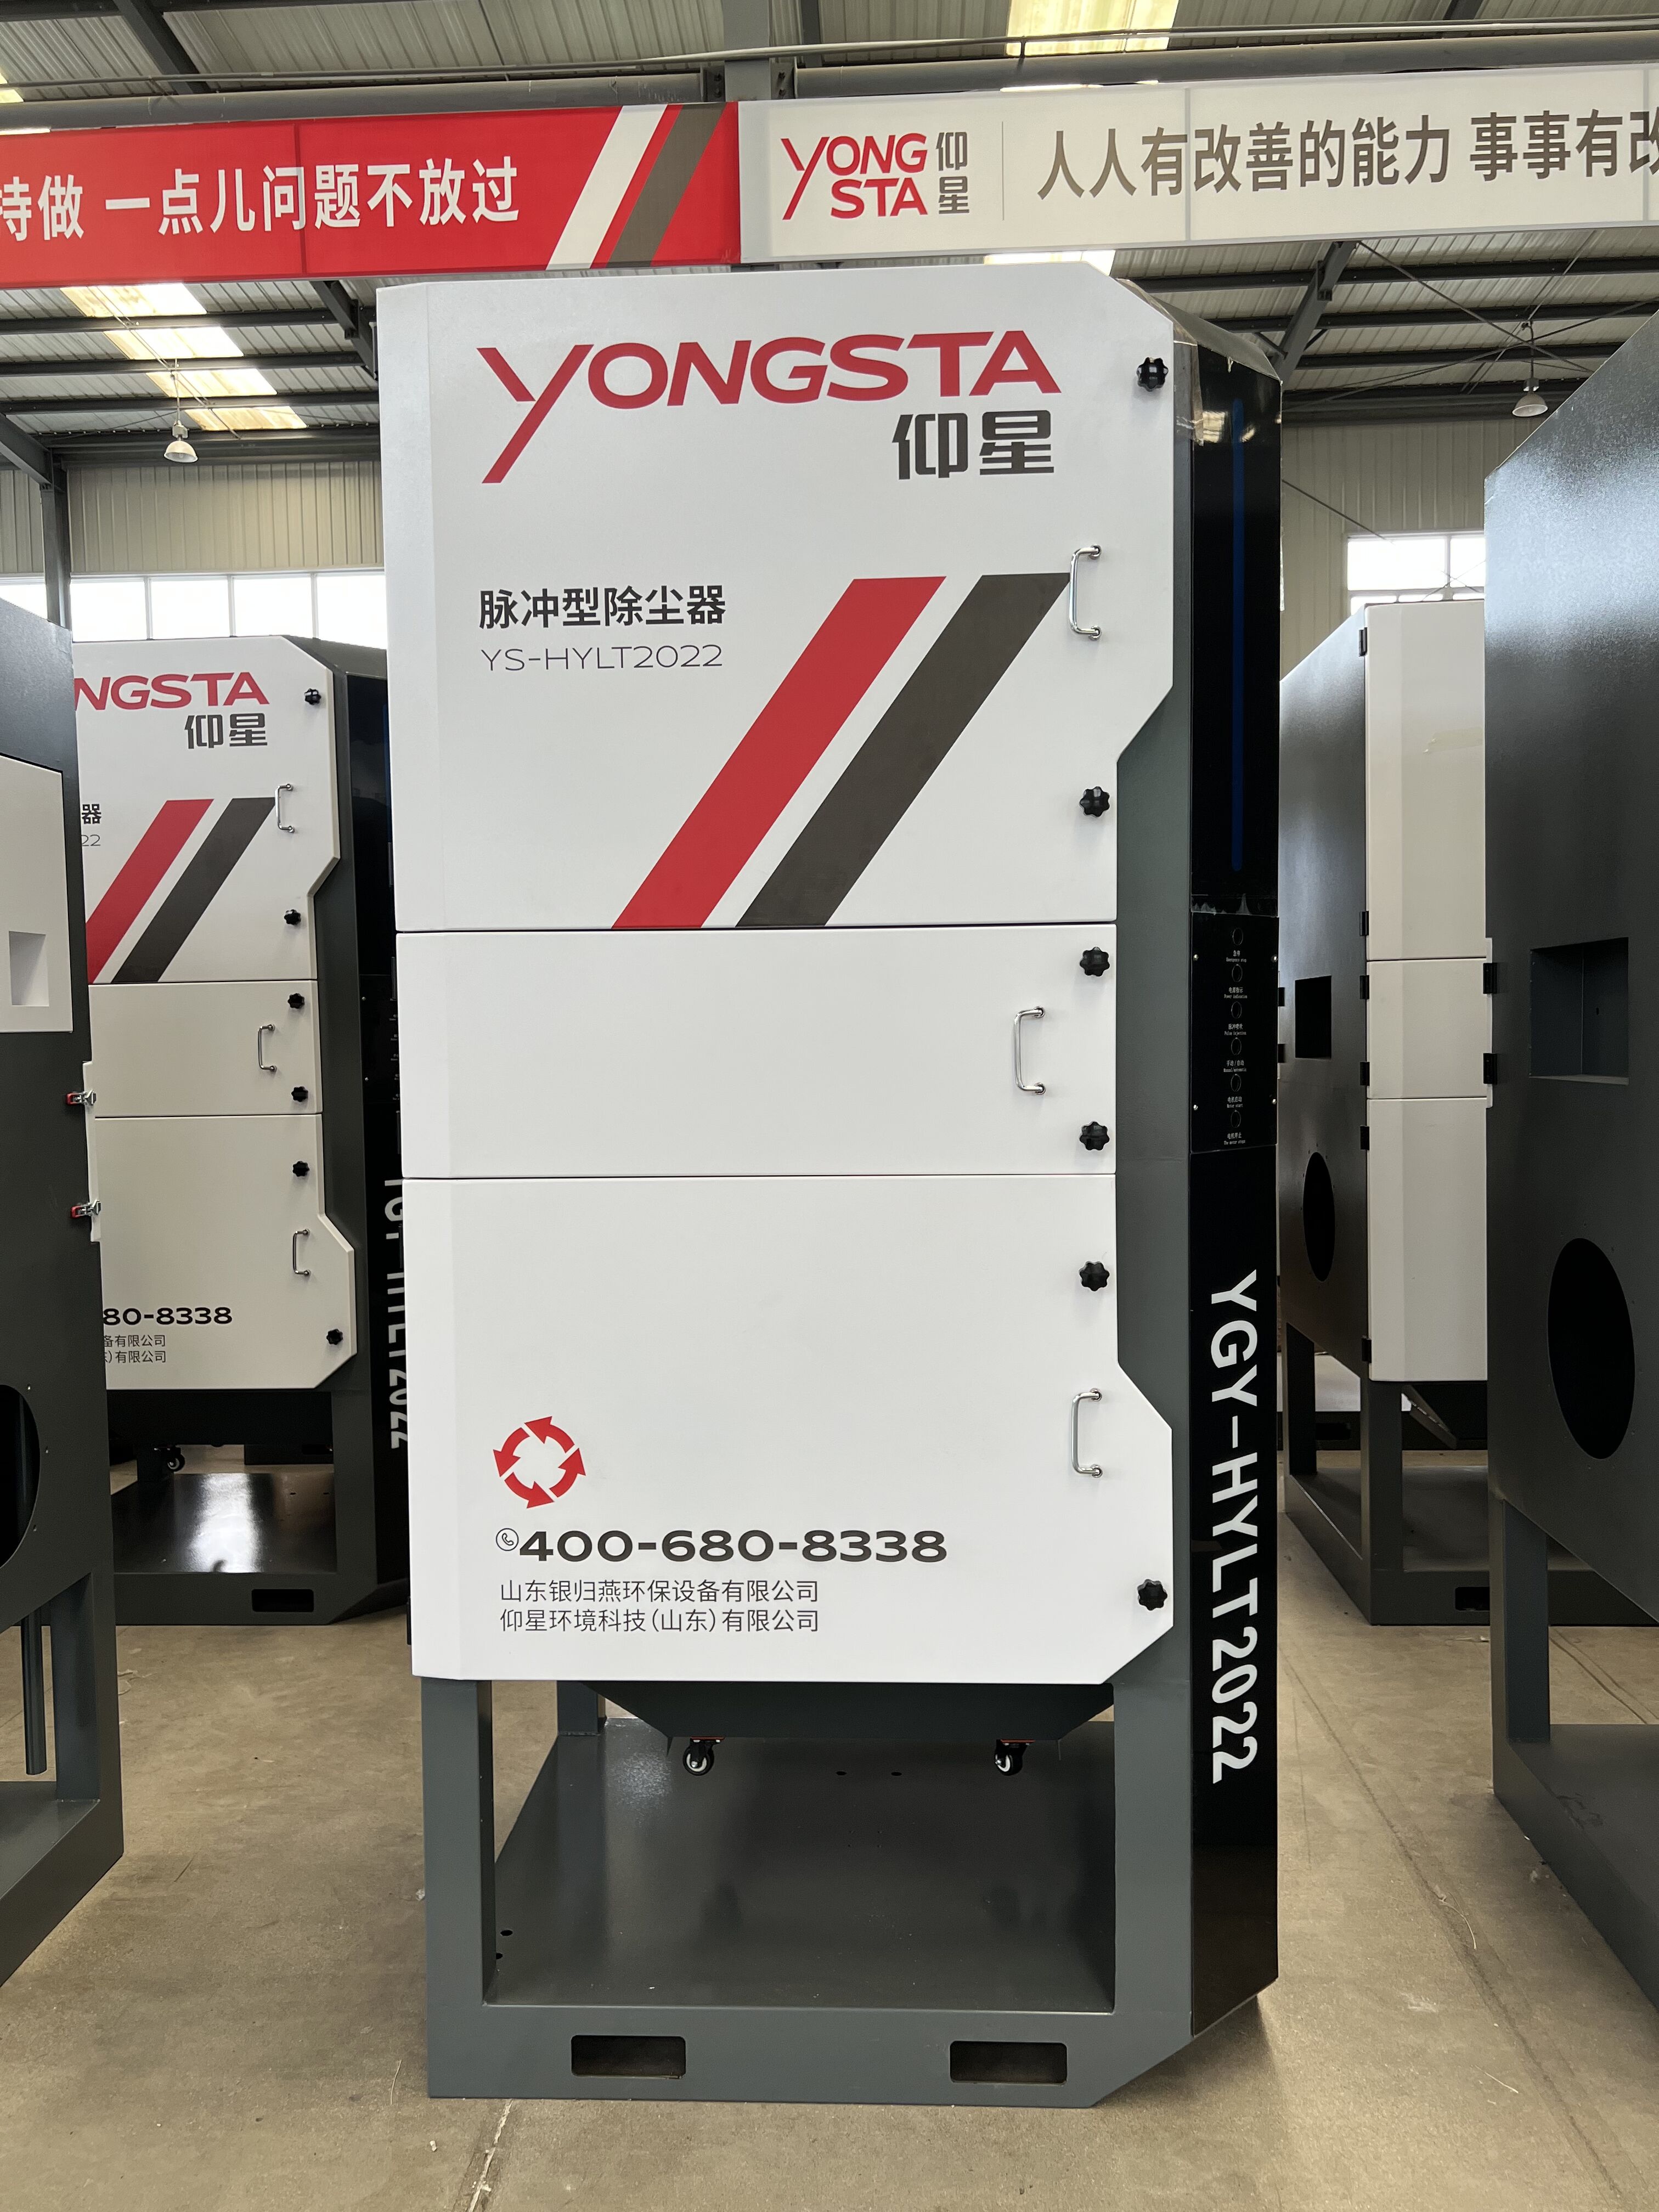
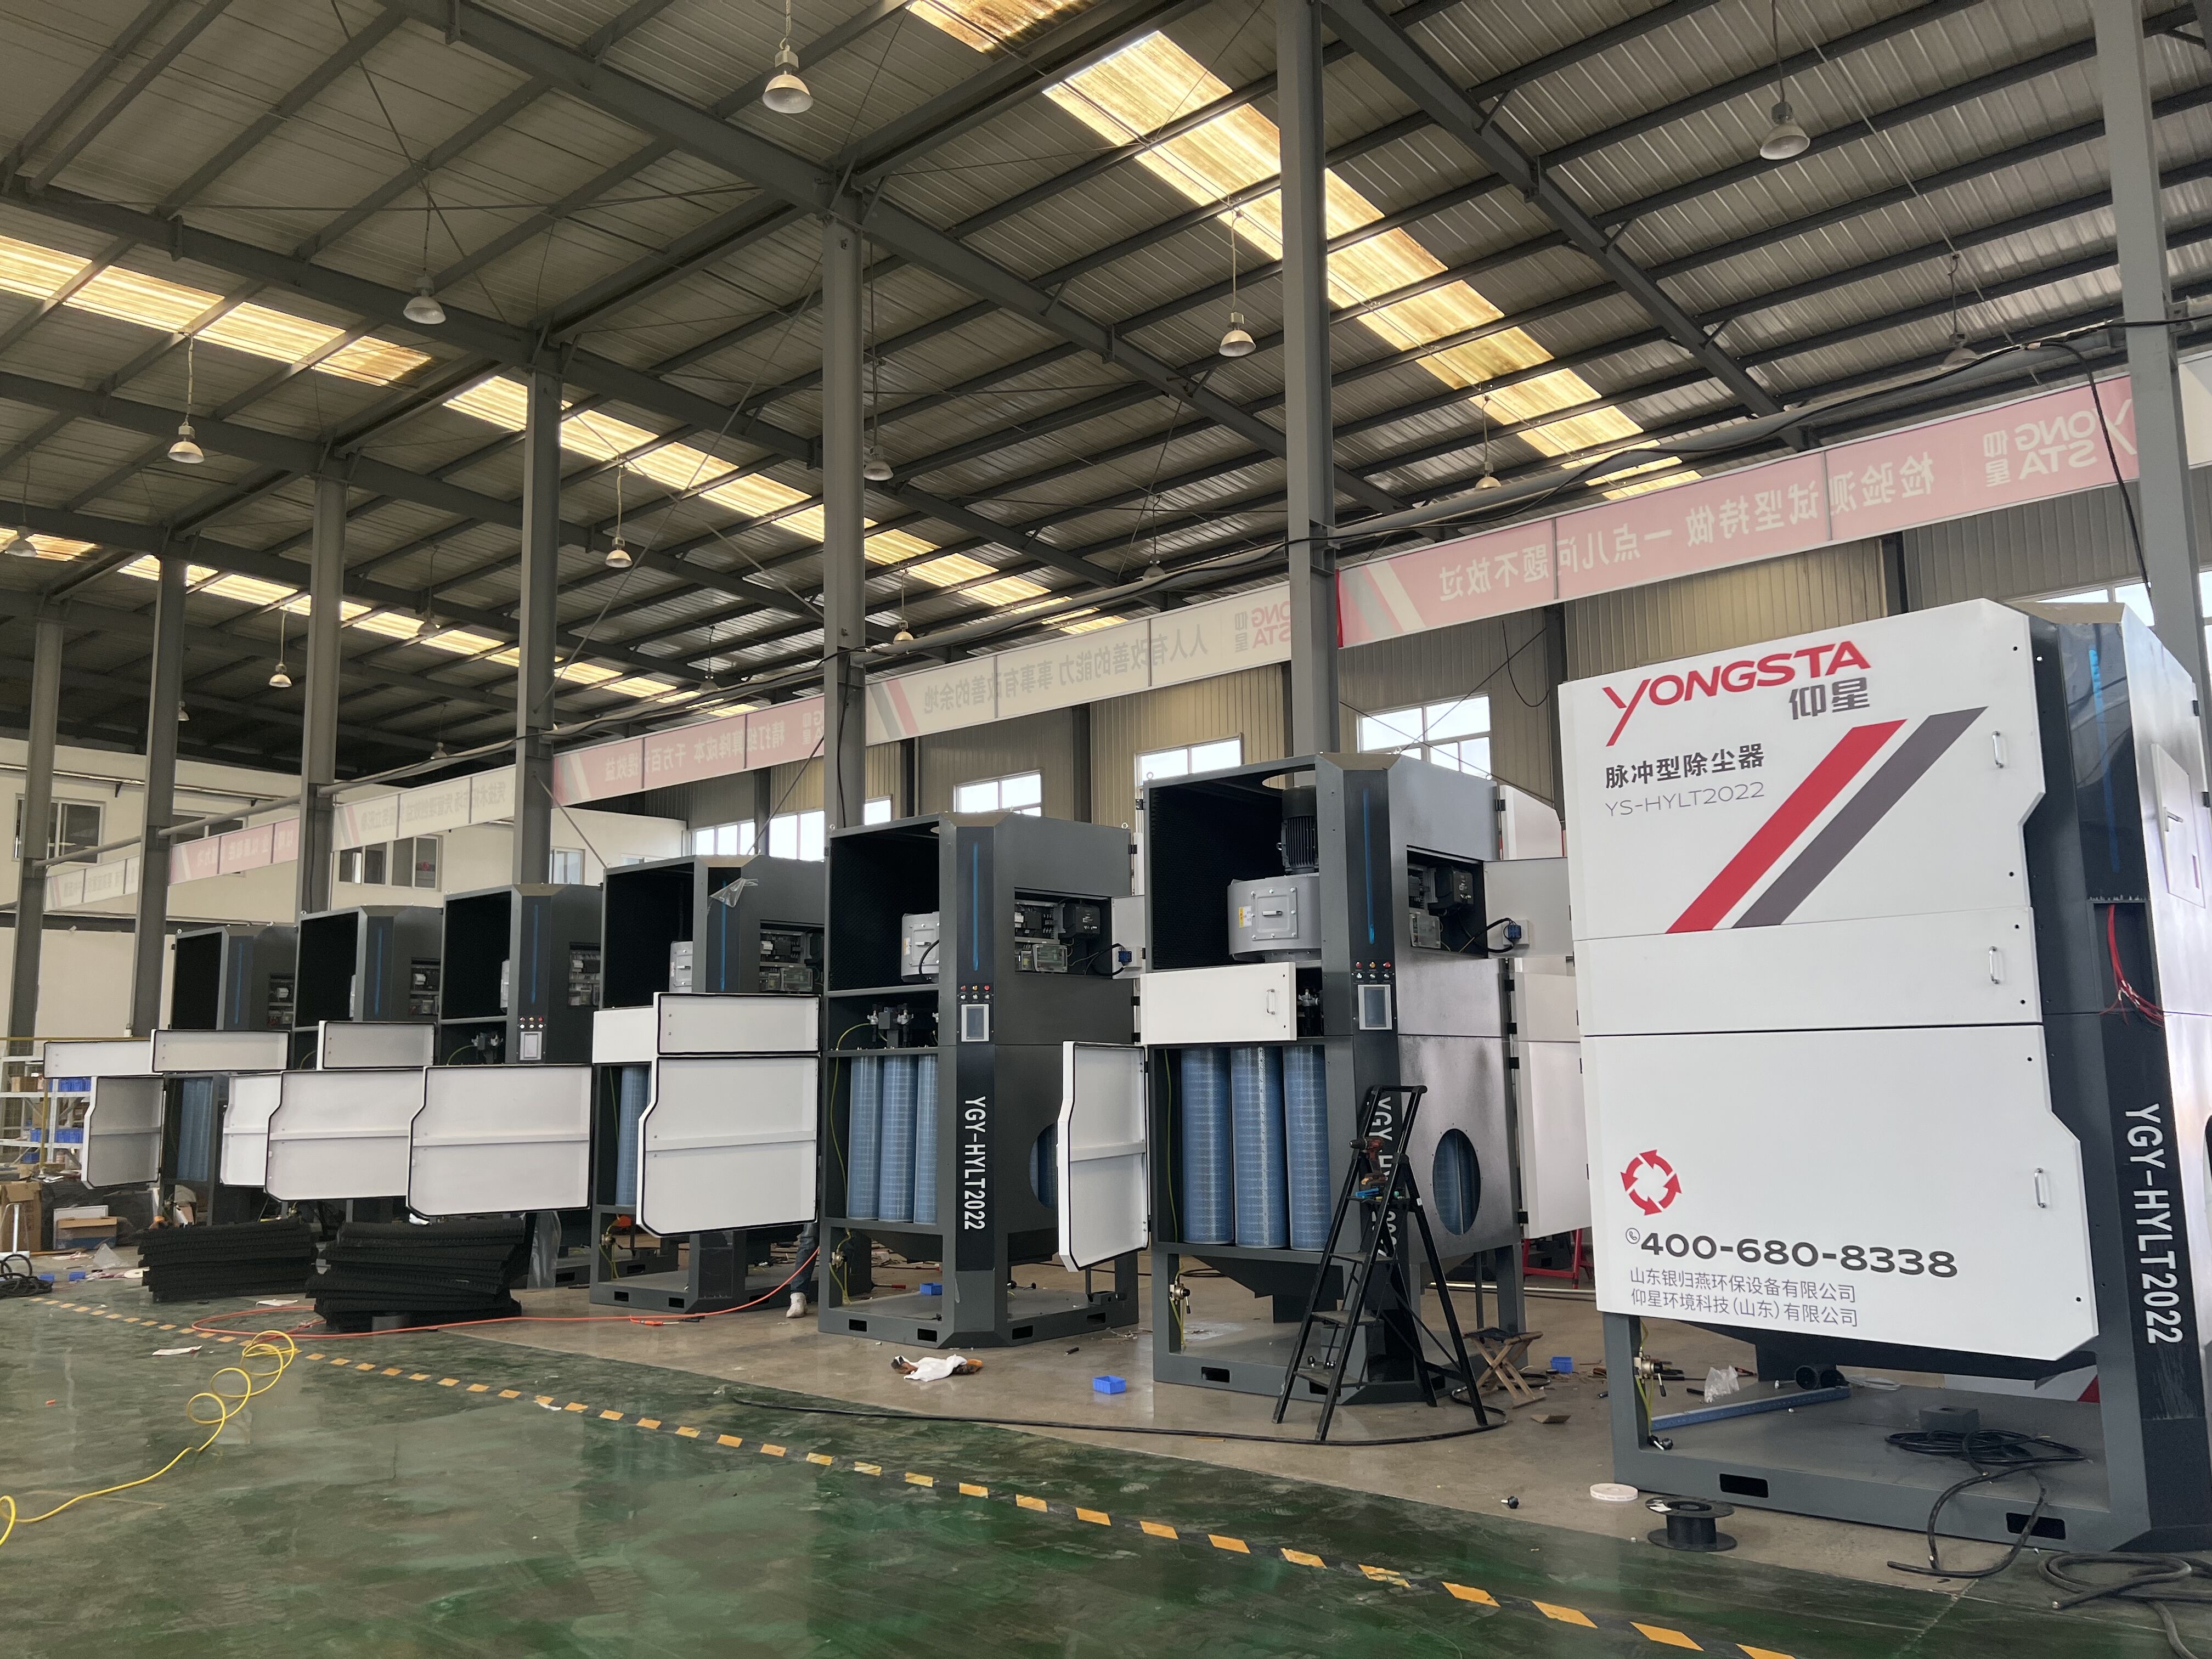
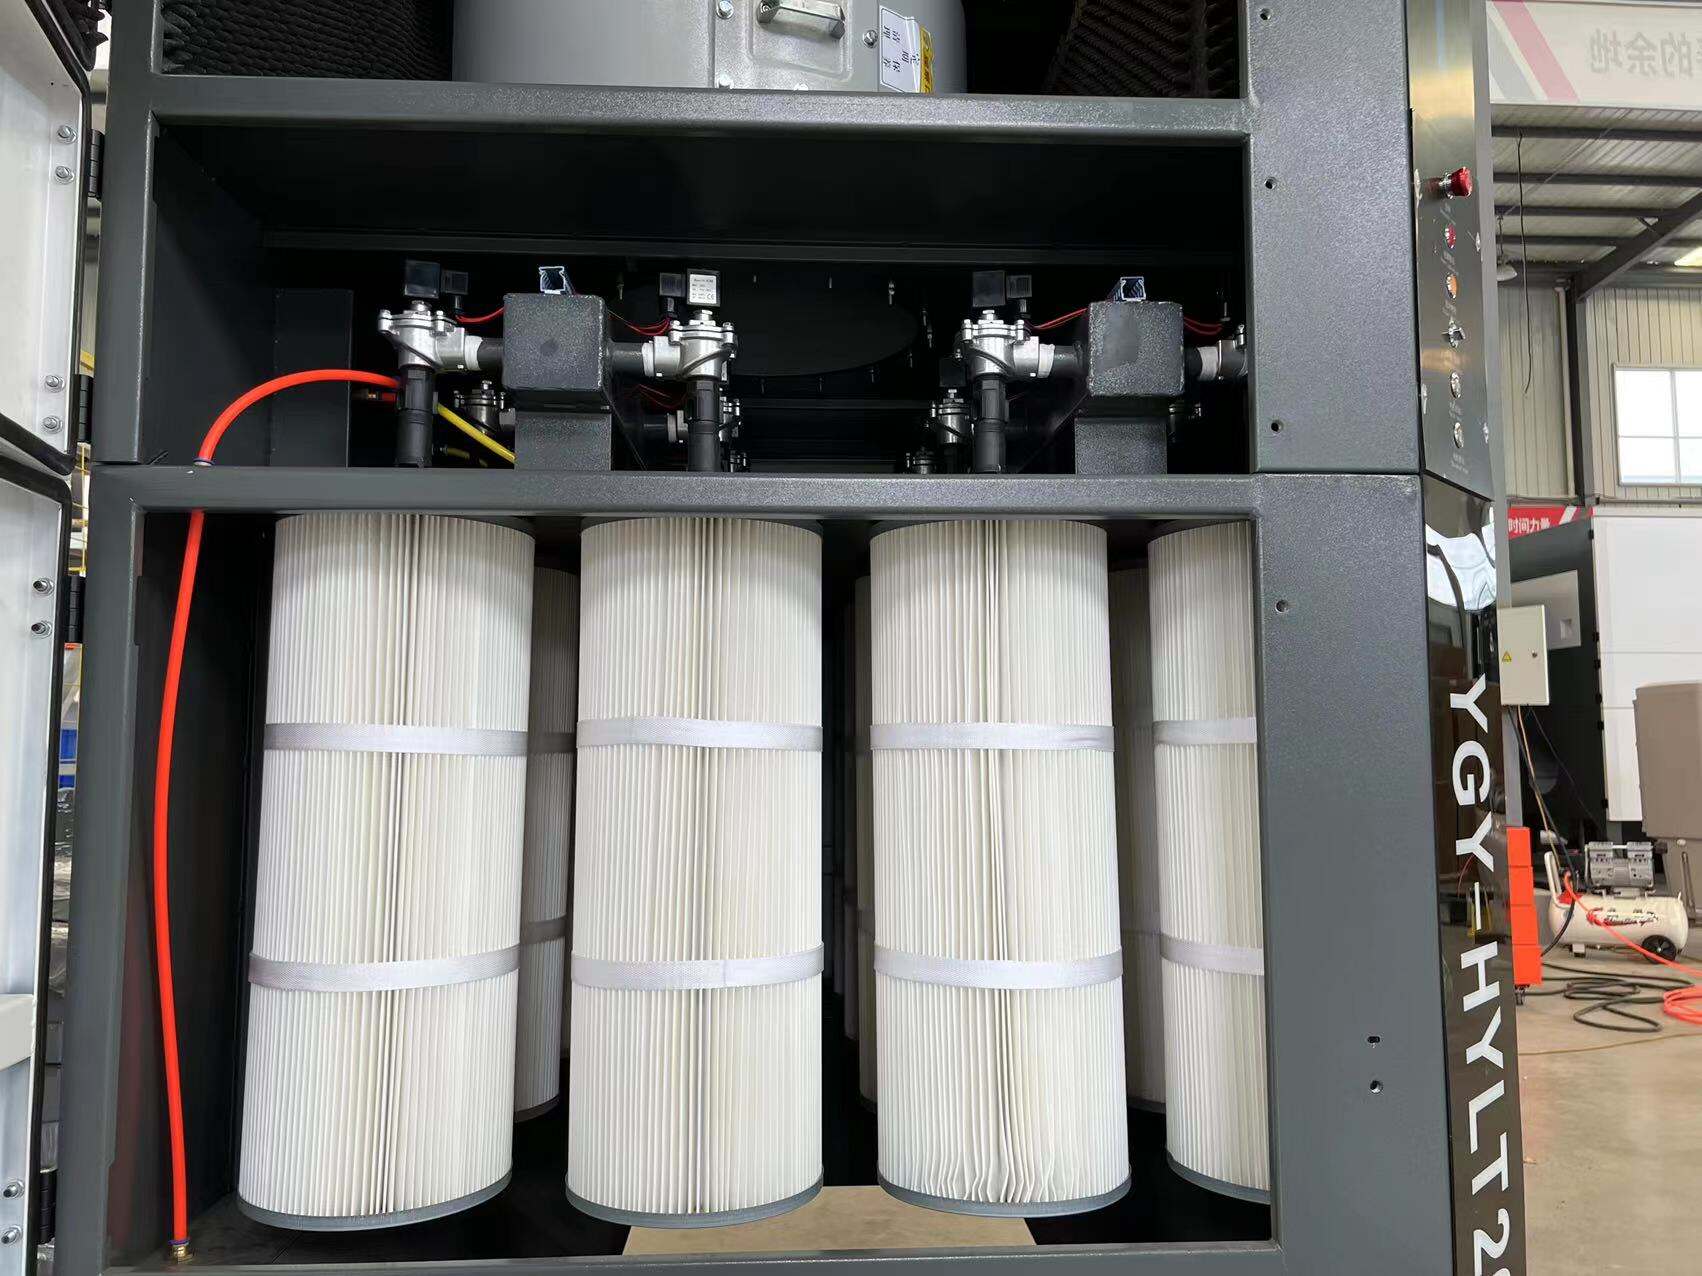
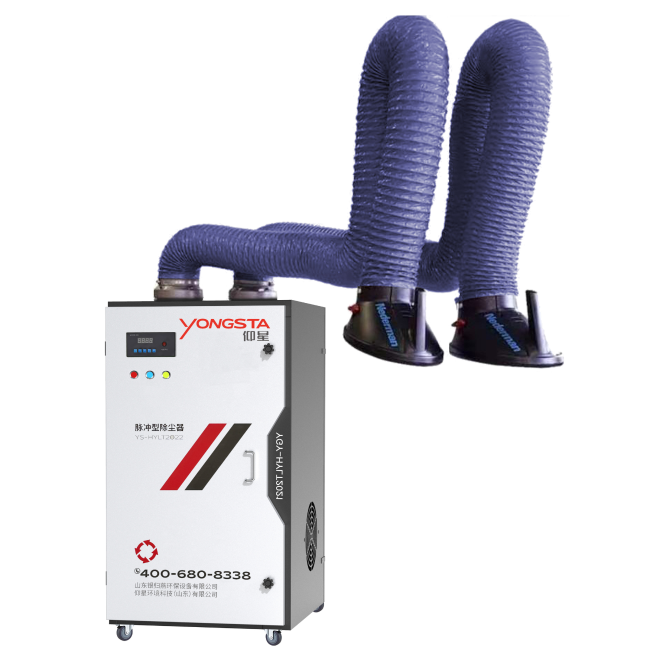
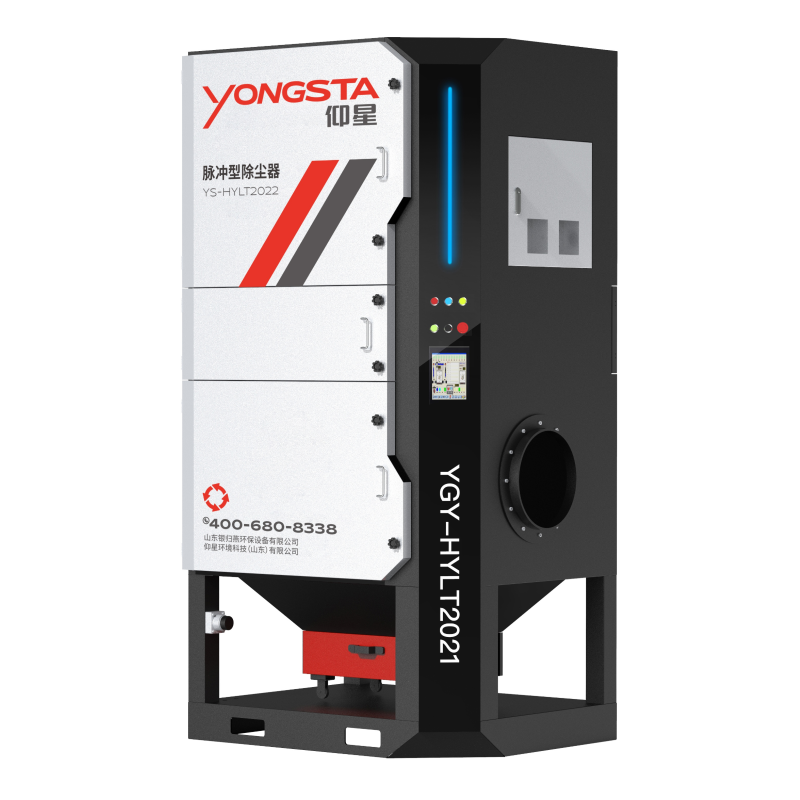
A cartridge filter dust collector represents an advanced air filtration system designed to capture and remove airborne particulates from industrial environments. This equipment utilizes pleated filter cartridges as its primary filtration media, offering superior dust collection capabilities across manufacturing facilities, workshops, and processing plants. The cartridge filter dust collector operates by drawing contaminated air through specialized filter elements that trap particles while allowing clean air to pass through and return to the workspace or exhaust outdoors. These systems feature a compact footprint compared to traditional baghouse collectors, making them ideal for facilities with limited floor space. The core technology revolves around cylindrical or conical filter cartridges constructed from spunbond polyester, cellulose, or nanofiber materials, each offering different filtration efficiencies and dust-holding capacities. Modern cartridge filter dust collector units incorporate pulse-jet cleaning mechanisms that automatically remove accumulated dust from filter surfaces, extending filter life and maintaining consistent airflow. The cleaning process uses compressed air bursts directed at individual cartridges, dislodging dust particles that fall into collection hoppers below. Applications span metalworking operations, woodworking shops, pharmaceutical manufacturing, food processing, chemical production, and powder coating facilities. The cartridge filter dust collector excels at capturing fine particulates ranging from sub-micron sizes to larger debris, protecting worker health and ensuring compliance with air quality regulations. Installation flexibility allows for both indoor and outdoor mounting configurations, with options for centralized systems serving multiple dust sources or standalone units dedicated to specific machines. Advanced models feature variable frequency drives for energy optimization, differential pressure monitoring for filter condition assessment, and explosion-proof designs for combustible dust environments. The modular construction of cartridge filter dust collector systems enables easy capacity expansion by adding filter modules as production demands increase. These collectors effectively handle dry dust applications while maintaining high collection efficiency throughout their operational cycle, making them essential equipment for maintaining clean industrial atmospheres and protecting valuable production equipment from abrasive particle damage.

New Product Releases

The cartridge filter dust collector delivers exceptional filtration performance while reducing operational costs and maintenance requirements compared to older dust collection technologies. These systems provide significantly larger filtration surface area within a smaller physical footprint, allowing facilities to maximize floor space for productive operations rather than dedicating excessive room to air quality equipment. The pleated design of filter cartridges creates more media surface area than flat filters or fabric bags of similar dimensions, resulting in lower air-to-media ratios and improved particle capture efficiency. This design advantage translates directly into energy savings, as the system requires less fan power to move air through the filters while maintaining effective dust removal. Maintenance becomes simpler and faster with cartridge filter dust collector technology because replacing filter elements takes minutes rather than hours, minimizing production downtime and reducing labor costs associated with filter changes. The cartridges install and remove without requiring workers to enter the collector housing, improving safety and eliminating confined space entry procedures. Automated pulse-jet cleaning extends filter service life by continuously removing dust buildup, allowing the cartridge filter dust collector to operate longer between filter replacements and reducing consumable costs over the equipment lifespan. The cleaning system operates on-demand based on differential pressure readings, ensuring filters receive cleaning only when necessary rather than on fixed schedules, further optimizing compressed air consumption. Environmental benefits include reduced waste generation since cartridge filters typically last longer than traditional bag filters, and many cartridge materials are recyclable at end of life. The cartridge filter dust collector operates quietly compared to older cyclone separators or high-velocity systems, creating a more comfortable work environment and reducing noise pollution concerns. Versatility stands out as another key advantage, with cartridge filter dust collector units handling diverse dust types from fine powders to fibrous materials without requiring extensive modifications. The systems adapt easily to changing production requirements through simple filter media changes, allowing the same collector to serve different applications as manufacturing needs evolve. Initial investment costs often prove lower than comparable baghouse installations due to simpler structural requirements and reduced installation complexity. Operating visibility improves through integrated monitoring systems that provide real-time performance data, enabling predictive maintenance scheduling and preventing unexpected failures. The compact design of cartridge filter dust collector equipment reduces shipping costs and simplifies installation in existing facilities where space constraints limit equipment options. Temperature tolerance varies by filter media selection, with specialized cartridges available for elevated temperature applications up to 350 degrees Fahrenheit, expanding the range of processes these collectors can serve effectively.

Latest News

Yongsta R&D Team Wins 3 Dust Removal Technology Patents, Leading Industry Innovation

09

Apr

Yongsta R&D Team Wins 3 Dust Removal Technology Patents, Leading Industry Innovation

View More
Yongsta Cooperates with TUV for ATEX Explosion-Proof Certification, Explosion-Proof Dust Collector to Be Launched Soon

09

Apr

Yongsta Cooperates with TUV for ATEX Explosion-Proof Certification, Explosion-Proof Dust Collector to Be Launched Soon

View More
Empowering Benchmark Manufacturing! Yongsta Cartridge Dust Collector Aids Siemens Transformer China Factory's Dust Removal Renovation and Gains High Recognition

09

Apr

Empowering Benchmark Manufacturing! Yongsta Cartridge Dust Collector Aids Siemens Transformer China Factory's Dust Removal Renovation and Gains High Recognition

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

cartridge filter dust collector

Superior Filtration Efficiency with Advanced Media Technology

Superior Filtration Efficiency with Advanced Media Technology

The cartridge filter dust collector achieves outstanding particle capture rates through sophisticated filter media engineering that combines multiple filtration mechanisms into a single compact element. Modern cartridge filters utilize nanofiber technology layered onto traditional substrate materials, creating a surface filtration barrier that captures particles on the filter face rather than allowing them to penetrate deep into the media structure. This surface loading characteristic means the cartridge filter dust collector maintains consistent airflow and pressure drop throughout its service life, unlike depth-loading filters that gradually restrict airflow as particles embed within the media. The pleated configuration maximizes filtration surface area, with a single cartridge providing up to 300 square feet of media in a package measuring just 12 inches in diameter and 26 inches in height. This space efficiency allows the cartridge filter dust collector to deliver high airflow capacity while occupying minimal floor space, making it ideal for crowded production environments where every square foot matters. The filtration efficiency reaches 99.9 percent for particles as small as 0.3 microns, effectively capturing respirable dust that poses the greatest health risks to workers while also protecting sensitive equipment from abrasive particle damage. Different media options allow the cartridge filter dust collector to handle specific dust characteristics, with cellulose cartridges excelling at fine powder collection, spunbond polyester managing general industrial dusts, and specialized nanofiber cartridges tackling submicron particles in pharmaceutical or electronics manufacturing. The filter media resists moisture absorption better than traditional fabric bags, preventing the formation of dust cakes that can blind filter surfaces and reduce collection efficiency. Static dissipative and flame-retardant media options make the cartridge filter dust collector suitable for combustible dust applications, providing essential safety features for facilities processing metal powders, wood dust, or organic materials. The cartridge design eliminates the need for internal support cages required by bag filters, reducing potential failure points and simplifying maintenance procedures. Filter cartridges maintain their structural integrity under pulse-jet cleaning, withstanding thousands of cleaning cycles without degradation, which extends service life and reduces replacement frequency. The cartridge filter dust collector benefits from continuous media technology improvements, with manufacturers regularly introducing enhanced materials that offer better performance, longer life, or specialized capabilities for emerging applications.
Intelligent Automated Cleaning System for Continuous Operation

Intelligent Automated Cleaning System for Continuous Operation

The cartridge filter dust collector incorporates sophisticated pulse-jet cleaning technology that automatically maintains optimal filter performance without manual intervention or production interruptions. This cleaning system uses precisely timed bursts of compressed air directed through venturi nozzles positioned above each filter cartridge, creating a shockwave that flexes the filter media and dislodges accumulated dust particles. The dislodged material falls into collection hoppers below, where it can be removed through rotary valves or manual cleanout doors depending on system configuration. Unlike older shaker-type cleaning mechanisms that require the collector to shut down during cleaning cycles, the pulse-jet system in a cartridge filter dust collector operates while the unit continues filtering, ensuring uninterrupted dust capture and consistent negative pressure at collection points. The cleaning controller monitors differential pressure across the filters, triggering cleaning sequences only when pressure drop reaches predetermined thresholds, which optimizes compressed air usage and extends filter life by avoiding unnecessary cleaning cycles. Advanced cartridge filter dust collector models feature programmable logic controllers that allow operators to customize cleaning parameters including pulse duration, pressure intensity, and interval timing to match specific dust characteristics and operational requirements. Sequential cleaning patterns ensure only a small portion of filters undergo cleaning at any moment, maintaining overall system airflow and collection efficiency throughout the cleaning process. The pulse-jet system proves particularly effective at removing sticky or cohesive dusts that might blind other filter types, making the cartridge filter dust collector suitable for challenging applications involving hygroscopic materials or dusts with high moisture content. Compressed air consumption remains minimal, typically requiring only 90 PSI supply pressure and consuming air only during brief pulse events lasting milliseconds, resulting in lower operating costs compared to continuous reverse-air cleaning systems. The cleaning effectiveness of a cartridge filter dust collector directly impacts filter service life, with properly tuned systems extending cartridge life by preventing excessive dust buildup that can permanently embed in filter media. Maintenance requirements for the cleaning system itself remain minimal, with solenoid valves and diaphragm assemblies representing the primary wear components that require periodic inspection and replacement. The cartridge filter dust collector cleaning system can be monitored remotely through industrial control networks, allowing maintenance personnel to track cleaning frequency, identify filters requiring replacement, and diagnose performance issues before they impact production operations.
Flexible Modular Design for Scalable Dust Control Solutions

Flexible Modular Design for Scalable Dust Control Solutions

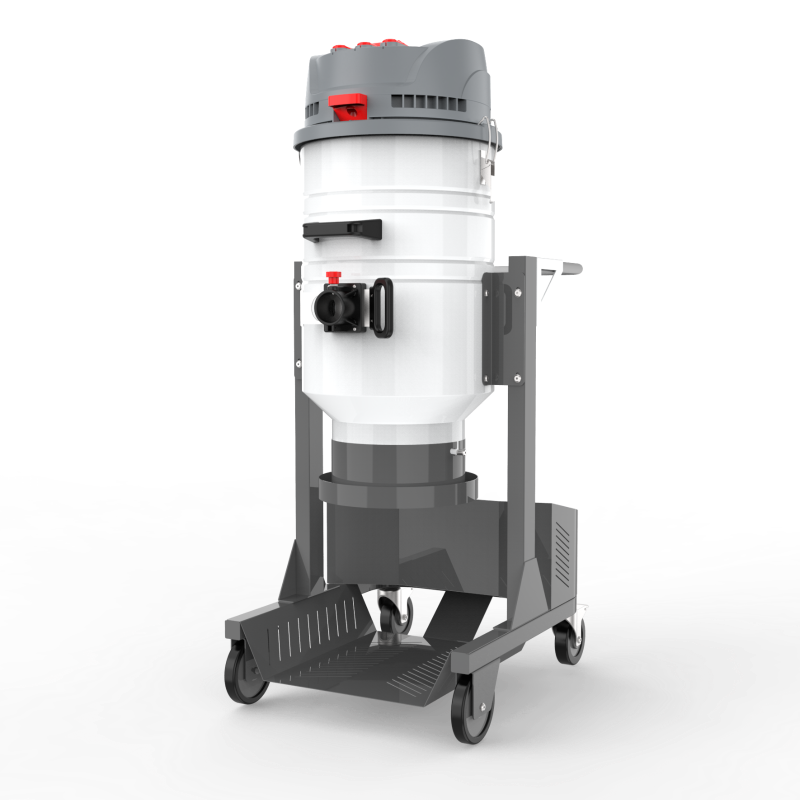
The cartridge filter dust collector offers unmatched installation flexibility and expansion capability through modular construction that adapts to evolving facility requirements and production changes. Manufacturers design these systems with standardized filter modules that can be combined in various configurations to achieve desired airflow capacities ranging from small standalone units handling 1,000 CFM to large centralized systems processing over 50,000 CFM. This scalability allows facilities to right-size their dust collection investment, starting with capacity matching current needs and adding modules as production expands rather than over-purchasing equipment upfront. The modular approach of a cartridge filter dust collector simplifies installation by breaking large systems into manageable components that fit through standard doorways and can be assembled on-site without requiring specialized rigging equipment or building modifications. Horizontal and vertical configurations provide layout flexibility, with horizontal models offering easy filter access for facilities with height restrictions and vertical designs minimizing floor space consumption in buildings with adequate ceiling clearance. The cartridge filter dust collector can be positioned indoors to recirculate heated or cooled air back to the workspace, reducing energy costs associated with conditioning makeup air, or installed outdoors to conserve interior space and simplify ductwork routing. Inlet configurations accommodate single or multiple dust sources, with manifold designs allowing one cartridge filter dust collector to serve numerous machines or process points through a centralized collection system. Explosion venting options integrate seamlessly into modular designs, providing essential safety features for combustible dust applications without requiring custom engineering or extensive modifications. The standardized construction of cartridge filter dust collector components means replacement parts remain readily available from manufacturers and distributors, reducing downtime risks and simplifying long-term maintenance planning. Upgrading older dust collection systems to cartridge filter dust collector technology often requires minimal structural changes, as the compact footprint typically fits within existing equipment footprints while delivering superior performance. Mobility options include caster-mounted portable units that can be relocated between workstations as production requirements change, providing dust control flexibility for job shops and facilities with variable production layouts. The cartridge filter dust collector design accommodates various discharge configurations including direct return to workspace, ducted exhaust to outdoors, or connection to central exhaust systems, allowing integration with existing facility ventilation infrastructure. Future-proofing becomes inherent in modular cartridge filter dust collector systems, as technological improvements like enhanced filter media or more efficient cleaning components can be incorporated during routine maintenance without replacing entire systems.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
email goToTop