Cartridge Dust Collector Factory - Advanced Industrial Air Filtration Systems

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

cartridge dust collector factory

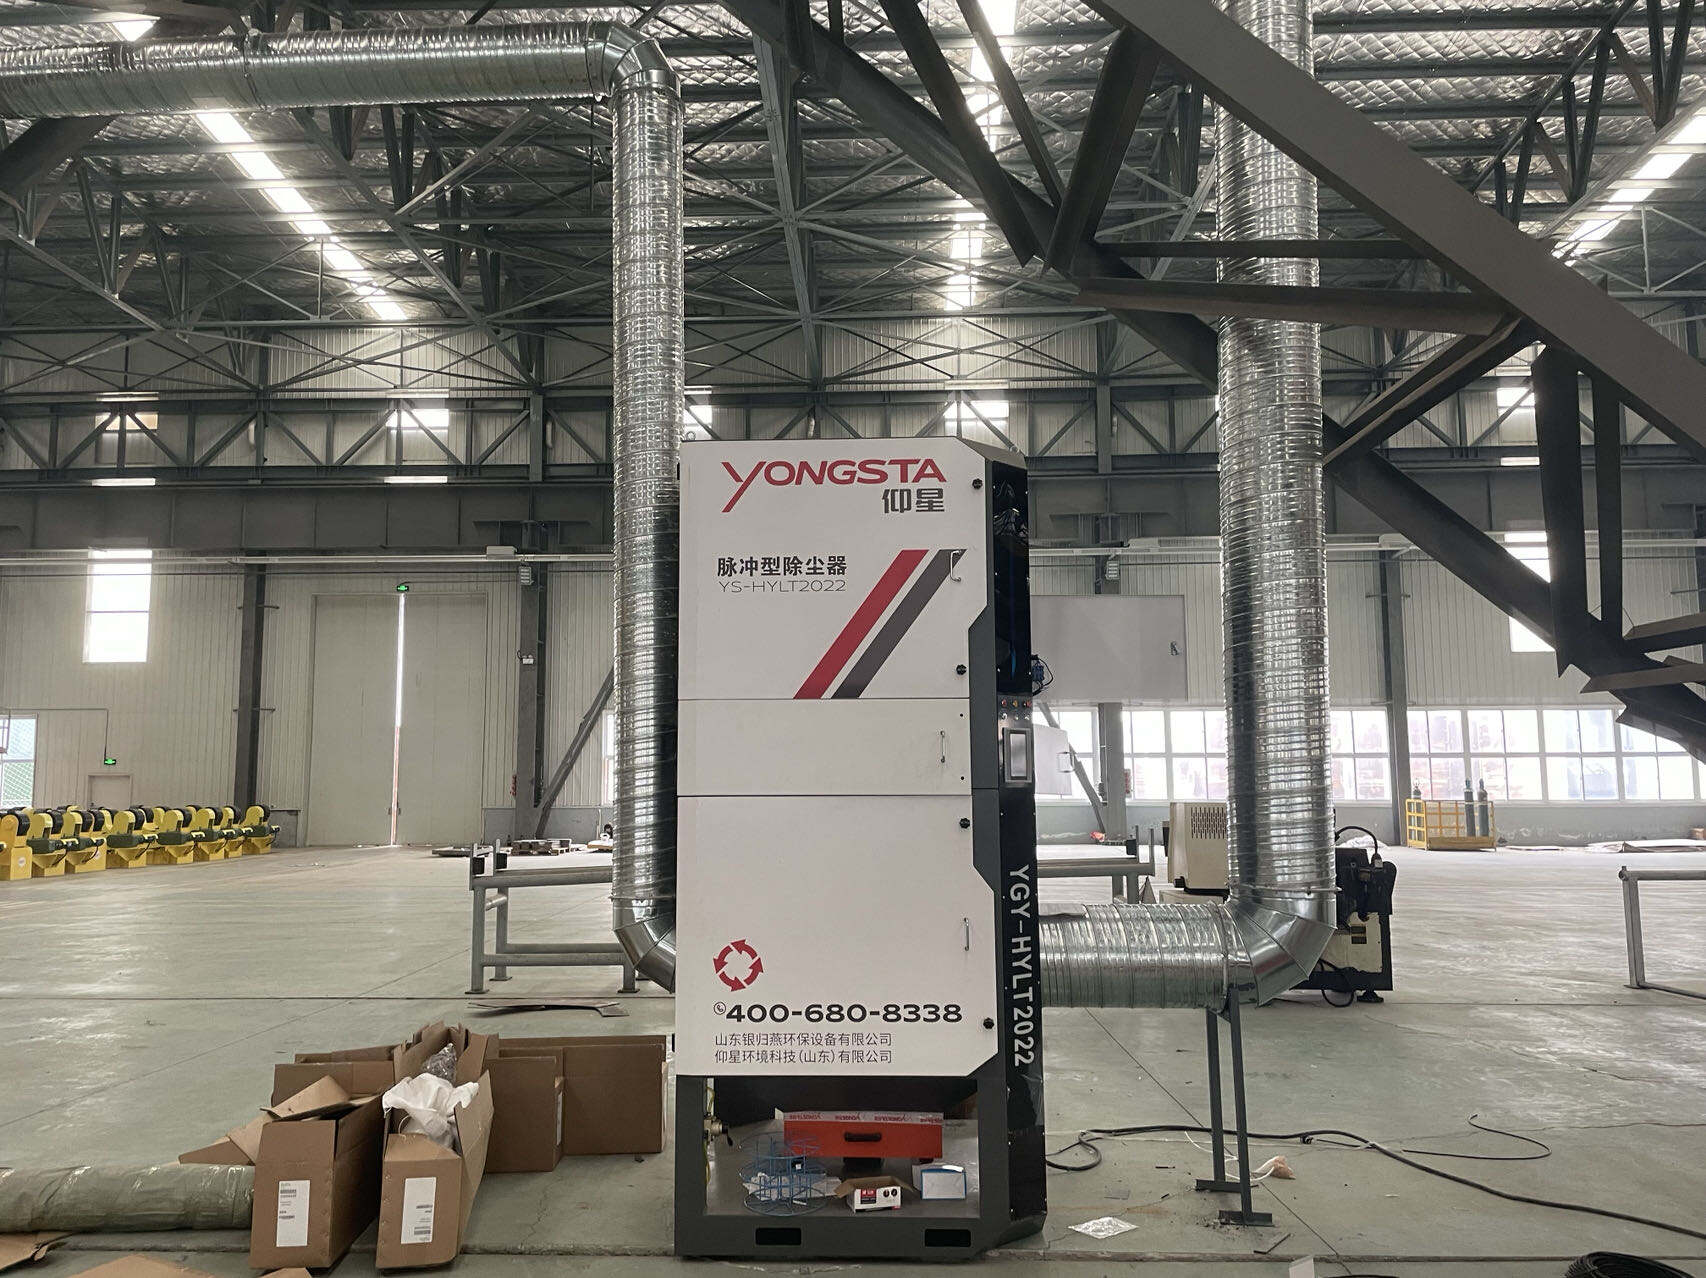
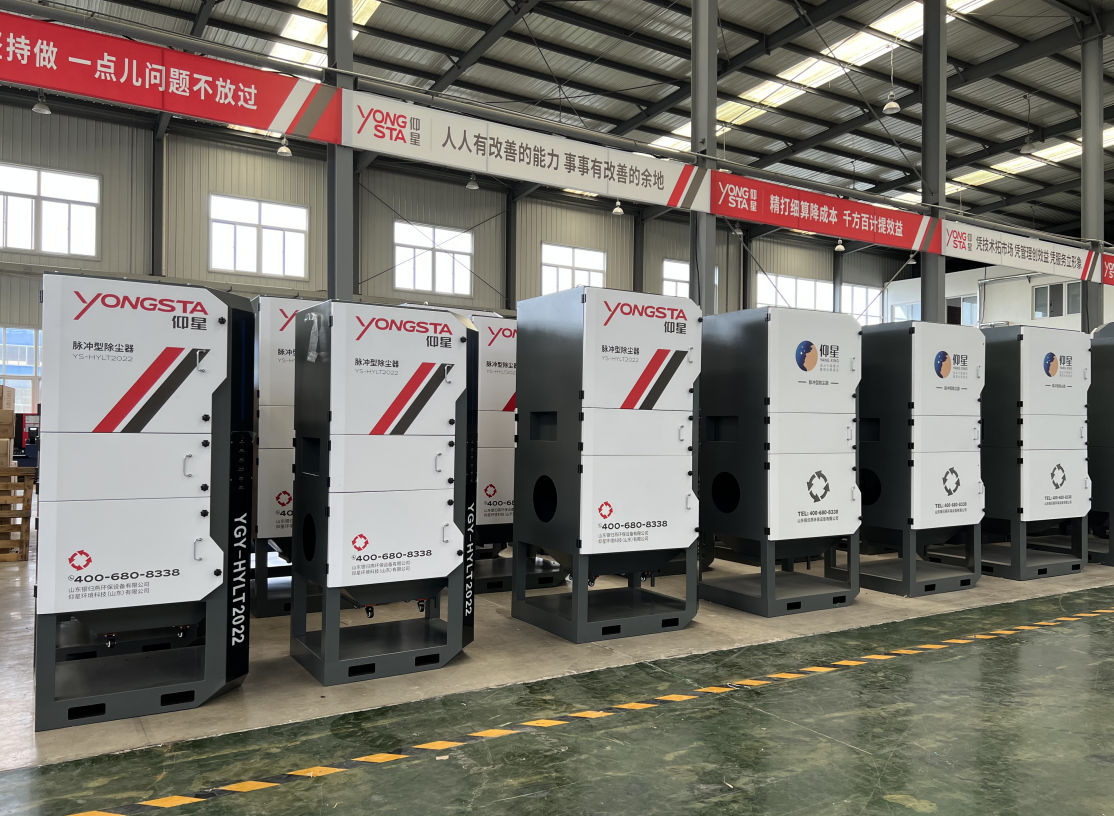
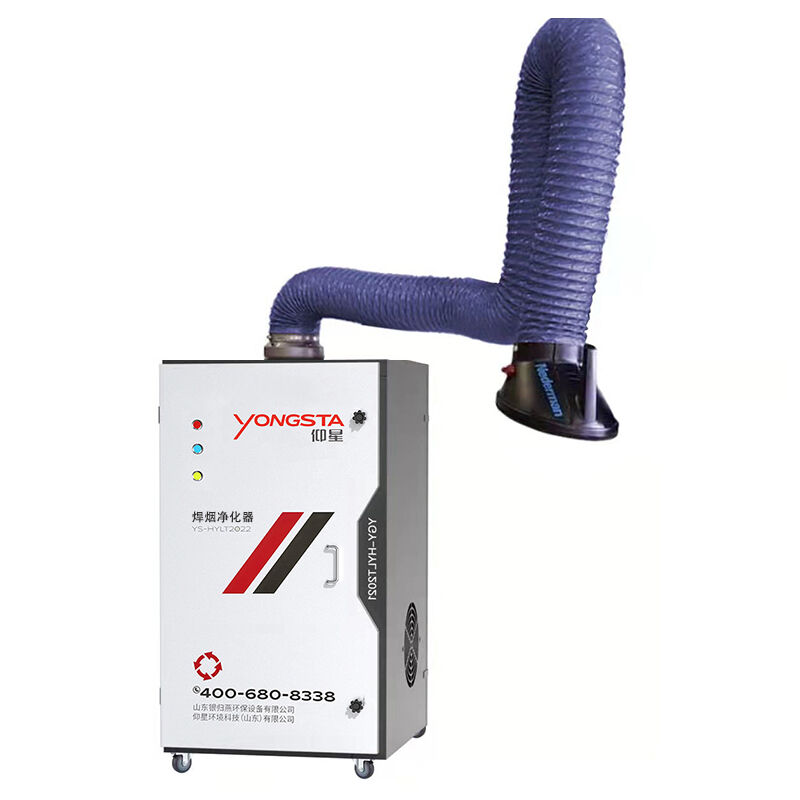
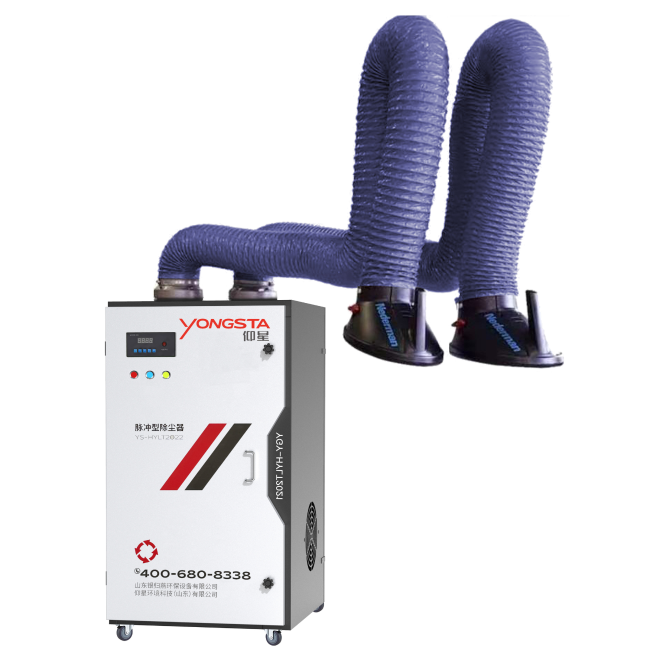
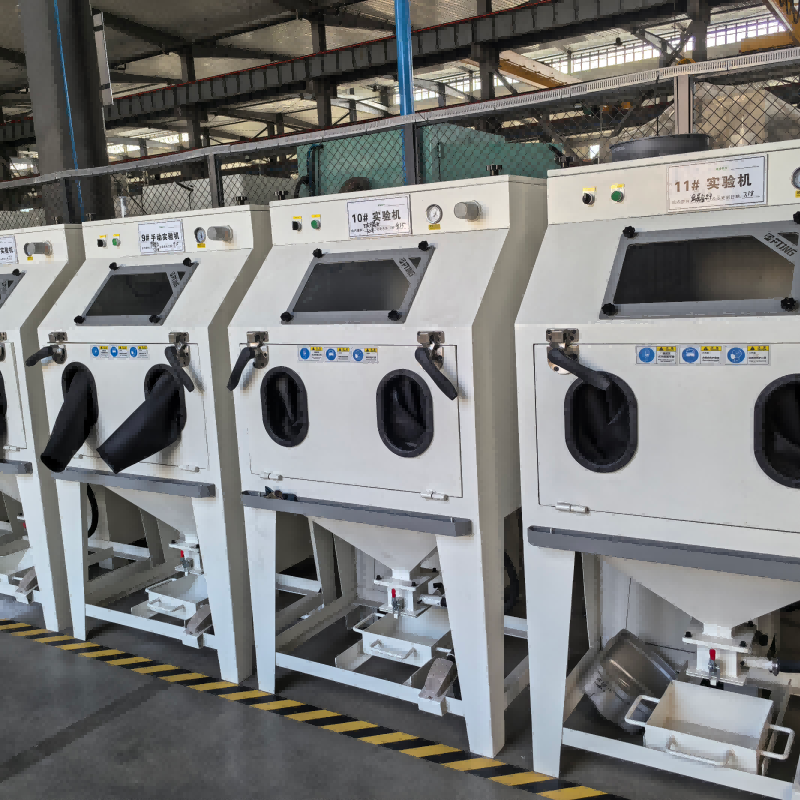
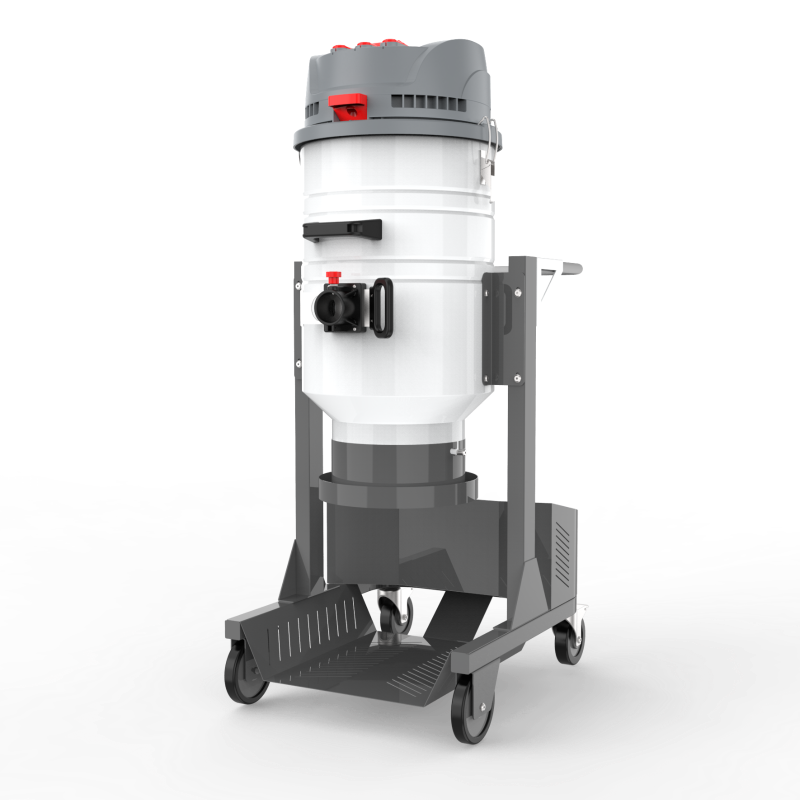
A cartridge dust collector factory specializes in manufacturing advanced air filtration systems designed to capture and remove airborne particulates from industrial environments. These facilities produce equipment that uses pleated filter cartridges as the primary filtration medium, offering superior dust collection capabilities across various manufacturing sectors. The cartridge dust collector factory focuses on creating systems that maintain clean air quality while ensuring compliance with environmental regulations and workplace safety standards. Modern production facilities incorporate cutting-edge engineering processes to develop collectors that feature compact designs, high filtration efficiency, and reduced maintenance requirements. The manufacturing process involves precision fabrication of housing units, integration of pulse-jet cleaning mechanisms, and assembly of filter cartridge arrays that maximize surface area for particle capture. These factories produce collectors suitable for applications ranging from metalworking and woodworking to pharmaceutical production and food processing. The technological infrastructure within a cartridge dust collector factory enables the creation of customized solutions tailored to specific industrial needs, including varying airflow capacities, filtration ratings, and explosion-proof configurations. Quality control measures ensure each unit meets stringent performance standards before deployment. The factory environment combines automated manufacturing processes with skilled craftsmanship to produce reliable dust collection systems that protect worker health, prevent equipment damage, and minimize environmental impact. By utilizing advanced materials and innovative design principles, the cartridge dust collector factory delivers products that offer extended filter life, energy-efficient operation, and simplified maintenance procedures, making them essential components in modern industrial facilities committed to maintaining clean production environments.

Popular Products

Choosing products from a cartridge dust collector factory brings numerous practical benefits that directly impact your operational efficiency and bottom line. First, these systems deliver exceptional filtration performance by capturing particles as small as 0.3 microns, which means cleaner air for your workers and reduced health risks associated with dust exposure. The compact footprint of cartridge-based systems allows you to save valuable floor space compared to traditional baghouse collectors, making them ideal for facilities with limited room for equipment installation. You will notice immediate energy savings because cartridge collectors operate at lower pressure drops, requiring less fan power to move air through the system. This translates to reduced electricity costs month after month. Maintenance becomes significantly easier since cartridge filters can be quickly replaced without specialized tools or extensive downtime, keeping your production lines running smoothly. The pulse-jet cleaning technology integrated into these systems automatically cleans filters during operation, extending their service life and reducing replacement frequency. You gain flexibility in system configuration because cartridge dust collector factory products can be designed as standalone units or integrated into existing ventilation systems. The modular construction allows for future expansion as your production needs grow. These collectors handle a wide range of dust types, from fine powders to fibrous materials, eliminating the need for multiple filtration systems. You benefit from reduced compressed air consumption during filter cleaning cycles compared to older technologies, further lowering operating costs. The sealed design prevents dust re-entrainment, ensuring captured particles stay contained rather than escaping back into your workspace. Fire and explosion protection features can be incorporated for applications involving combustible dusts, providing critical safety measures. The durable construction using corrosion-resistant materials ensures long equipment life even in harsh industrial environments. You receive systems that comply with environmental regulations, helping you avoid fines and maintain good standing with regulatory agencies. The cartridge dust collector factory approach emphasizes user-friendly controls and monitoring systems that provide real-time performance data, enabling proactive maintenance and optimizing system efficiency. Overall, these advantages combine to deliver a dust collection solution that protects your workforce, preserves your equipment, reduces operational costs, and supports sustainable manufacturing practices.

Latest News

Yongsta R&D Team Wins 3 Dust Removal Technology Patents, Leading Industry Innovation

09

Apr

Yongsta R&D Team Wins 3 Dust Removal Technology Patents, Leading Industry Innovation

View More
Yongsta Cooperates with TUV for ATEX Explosion-Proof Certification, Explosion-Proof Dust Collector to Be Launched Soon

09

Apr

Yongsta Cooperates with TUV for ATEX Explosion-Proof Certification, Explosion-Proof Dust Collector to Be Launched Soon

View More
Empowering Benchmark Manufacturing! Yongsta Cartridge Dust Collector Aids Siemens Transformer China Factory's Dust Removal Renovation and Gains High Recognition

09

Apr

Empowering Benchmark Manufacturing! Yongsta Cartridge Dust Collector Aids Siemens Transformer China Factory's Dust Removal Renovation and Gains High Recognition

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

cartridge dust collector factory

Advanced Filtration Technology for Maximum Particle Capture

Advanced Filtration Technology for Maximum Particle Capture

The cartridge dust collector factory employs sophisticated filtration technology that sets industry standards for particle capture efficiency and air quality improvement. At the core of this technology lies the pleated cartridge design, which dramatically increases the available filtration surface area within a compact housing. Unlike traditional flat filters, the pleated configuration creates multiple layers of filtration media arranged in accordion-style folds, multiplying the effective filtering surface by factors of ten or more. This expanded surface area allows the system to capture higher volumes of dust while maintaining optimal airflow rates. The filter media itself consists of specialized materials engineered at the microscopic level to trap particles through multiple mechanisms including interception, impaction, and diffusion. Advanced cartridge dust collector factory products utilize nanofiber technology layered onto base substrates, creating an ultra-fine mesh that captures submicron particles with remarkable efficiency. This technology proves particularly valuable in industries where fine dust poses significant health risks or product contamination concerns. The filtration efficiency ratings often exceed 99.9 percent for particles in the respirable size range, providing protection that surpasses regulatory requirements. The cartridge dust collector factory integrates these high-performance filters into systems designed for consistent, reliable operation across varying dust loads and environmental conditions. The pulse-jet cleaning mechanism works in concert with the filtration technology, delivering precisely timed bursts of compressed air that dislodge accumulated dust from filter surfaces without damaging the delicate media. This automated cleaning process maintains consistent airflow and pressure drop throughout the operating cycle, preventing the performance degradation common in systems lacking effective cleaning mechanisms. The cartridge dust collector factory designs these cleaning systems with adjustable parameters, allowing customization based on specific dust characteristics and production schedules. The result is a filtration system that maintains peak performance over extended periods, reducing the frequency of filter replacements and associated maintenance costs. Furthermore, the cartridge dust collector factory incorporates differential pressure monitoring that tracks filter condition in real-time, alerting operators when cleaning cycles need adjustment or filters require replacement. This intelligent monitoring prevents premature filter changes while ensuring filters are never operated beyond their effective service life, optimizing both performance and cost-efficiency.
Energy-Efficient Design Reducing Operational Costs

Energy-Efficient Design Reducing Operational Costs

The cartridge dust collector factory prioritizes energy efficiency throughout the design and manufacturing process, creating systems that significantly reduce operational expenses while maintaining superior performance. Energy consumption represents one of the largest ongoing costs for industrial dust collection systems, making efficiency improvements directly impactful to your profitability. The cartridge dust collector factory achieves energy savings through multiple engineering innovations that work synergistically. The pleated cartridge design inherently operates at lower pressure drops compared to traditional bag filters, meaning the system fan requires less power to pull air through the filtration media. This reduced resistance translates to lower horsepower requirements and decreased electricity consumption during every hour of operation. Over the course of a year, these savings accumulate to substantial reductions in energy costs. The cartridge dust collector factory further enhances efficiency by optimizing airflow patterns within the collector housing, minimizing turbulence and pressure losses that waste energy. Computational fluid dynamics modeling during the design phase ensures smooth air distribution across all filter cartridges, preventing dead zones and maximizing the utilization of available filtration surface. Variable frequency drives can be integrated into cartridge dust collector factory systems, allowing fan speed adjustment based on actual dust loading and production demands rather than running continuously at maximum capacity. This intelligent speed control reduces energy consumption during periods of lower dust generation while maintaining adequate capture velocity when production intensifies. The pulse-jet cleaning system itself demonstrates energy efficiency through optimized compressed air usage. The cartridge dust collector factory engineers cleaning sequences that deliver effective filter cleaning with minimal air consumption, using precisely calibrated valve timing and pressure settings. Modern systems incorporate on-demand cleaning triggered by differential pressure sensors rather than fixed time intervals, ensuring compressed air is used only when actually needed for filter maintenance. The cartridge dust collector factory also considers the total system energy profile, including the compressed air generation required for cleaning cycles. By minimizing cleaning frequency through superior filter design and optimizing each cleaning pulse for maximum effectiveness, the overall energy footprint decreases substantially. Insulated housing options available from the cartridge dust collector factory prevent heat loss in applications involving heated air streams, maintaining process temperatures and reducing heating costs. The combination of these energy-saving features creates a dust collection system with significantly lower lifetime operating costs compared to conventional alternatives, delivering return on investment through reduced utility expenses while supporting corporate sustainability initiatives and environmental responsibility goals.
Customizable Solutions for Diverse Industrial Applications

Customizable Solutions for Diverse Industrial Applications

The cartridge dust collector factory excels in providing customizable solutions that address the unique challenges present in diverse industrial environments, ensuring optimal performance regardless of application specifics. Manufacturing facilities vary dramatically in their dust collection requirements based on the materials processed, production volumes, available space, and regulatory constraints they face. Recognizing this diversity, the cartridge dust collector factory maintains flexible manufacturing capabilities that allow extensive customization of standard designs or complete custom engineering for specialized applications. The customization process begins with thorough application analysis, where cartridge dust collector factory engineers evaluate dust characteristics including particle size distribution, dust loading rates, chemical composition, temperature, moisture content, and combustibility properties. This comprehensive assessment informs every aspect of system design, from filter media selection to housing materials and safety features. For applications generating combustible dusts, the cartridge dust collector factory incorporates explosion venting, suppression systems, and spark detection equipment that comply with NFPA standards, protecting personnel and facilities from catastrophic events. When dealing with hygroscopic or sticky dusts that tend to blind filters, the cartridge dust collector factory specifies specialized filter media with surface treatments that resist cake buildup and facilitate easier cleaning. Temperature considerations lead to the selection of appropriate filter materials rated for elevated temperatures, with options ranging from standard cellulose blends to high-temperature synthetic fibers and even PTFE membranes for extreme conditions. The cartridge dust collector factory offers various housing configurations including indoor models, outdoor weatherproof units, and explosion-proof designs certified for hazardous locations. Capacity customization ensures the system matches your specific airflow requirements, with cartridge dust collector factory products available in sizes ranging from small portable units handling a few hundred CFM to large central systems processing tens of thousands of CFM. Multiple inlet configurations accommodate different ductwork layouts, while discharge options include filtered air return to the workspace for energy conservation or exhaust to atmosphere where required. The cartridge dust collector factory provides various control system options from basic manual operation to fully automated systems with PLC integration, remote monitoring capabilities, and data logging for compliance documentation. Special coatings and material upgrades address corrosive environments, while sanitary designs meet the stringent requirements of food, pharmaceutical, and medical device manufacturing. The cartridge dust collector factory approach to customization extends beyond initial equipment design to include ongoing support, spare parts availability, and system modifications as your production needs evolve, ensuring your dust collection investment continues delivering value throughout its operational life.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
email goToTop